
- Catalogs
- Tungaloy EUROPE
- GENERAL CATALOG-VOL.l

GENERAL CATALOG-VOL.l

GENERAL CATALOG-VOL.l
Tungaloy is a leader in the metal removal industry, offering cutting-edge innovations in grades and geometries for enhanced performance and tool life. Their latest cutting tools contribute to carbon neutrality.
This catalog provides information on Tungaloy’s cutting tools as of September 2022. Specifications may change without notice, and products may be discontinued as new developments arise. Dimensions are in millimeters, and indexable tools require separate orders for applicable inserts or heads.
Designations for tools include right- and left-hand options, indicated by R/L. For example, A16Q-STFPR/L13-D180 allows ordering both right- and left-hand tools. The catalog includes a lineup for inserts and solid tools, with a contact option for blank entries.
- Turning
- Grooving
- Threading
- Miniature Machining
- Drilling
- Milling
Toolholders are available with various approach angles and are suitable for negative 80° rhombic inserts. Specific torque recommendations are provided for clamping.
Inserts are categorized by application, grade, cutting conditions, and chipbreaker shape. Options are available for precision finishing, medium to heavy cutting, and more.
The catalog uses dimension symbols conforming to the ISO13399 standard, which standardizes electronic tool data globally. This includes 2D and 3D CAD data for integration into NC programs and CAM software.
2D and 3D CAD data are available in the e-catalog, with light and detailed types for tool path checking and new tool layout creation.
Tungaloy’s catalog is a comprehensive resource for selecting and ordering cutting tools, with a focus on innovation and sustainability in manufacturing.
- Toolholder lengths may not conform to ISO standards.
- Right-hand toolholders (R) should be used with left-hand inserts (L), and left-hand toolholders (L) with right-hand inserts (R).
Spare Parts and Accessories:
- Includes shims, clamping screws, wrenches, spring pins, levers, and optional oil supply attachments.
- Recommended clamping torque is specified for each toolholder.
Insert Selection and Applications:
- Inserts are categorized by application, grade, cutting conditions, and breaker shape.
- Applications range from precision finishing to medium and heavy cutting.
- Specific grades and chipbreaker shapes are recommended for different cutting conditions.
Toolholder and Insert Designations:
- Various toolholder models are listed with specifications such as diameter, length, and angle.
- Standard corner radius (RE) is provided for each insert.
Material and Grade Information:
- Materials include reinforced carbide and steel.
- Grades such as T515, NS9530, and AH6225 are mentioned for different applications.
Additional Notes:
- Lever-lock boring bars are available for negative rhombic inserts with specific approach angles.
- High-pressure coolant capability is noted for certain models.
- Reference pages and additional resources are available at tungaloy.com.
Catalog excerpts
turning grooving we improve, we evolve, we ADD
Open the catalog to page 1
Tungaloy’s Insights – Smart Manufacturing Tungaloy, as one of the leaders in the metal removal industry, offers the latest innovations in grades and geometries for superb performance and tool life. Tungaloy’s latest innovations in cutting tools contribute to carbon neutral
Open the catalog to page 3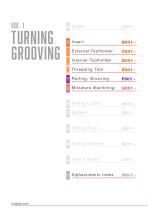
turning grooving Miniature Machining A lpha nume r ic Index
Open the catalog to page 4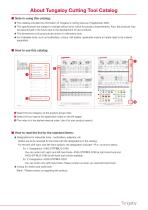
About Tungaloy Cutting Tool Catalog ■ Note in using this catalog: ★ This catalog provides the information of Tungaloy’s cutting tools as of September 2022. ★ The specifications are subject to change without prior notice for product improvements. Also, the products may be discontinued in the future due to the development of new products. ★ The dimensions of all products are shown in millimeters (mm). ★ For indexable tools, such as toolholders, cutters, drill bodies, applicable inserts or heads need to be ordered separately. Miniature Machining SPARE PARTS Designation C5PCLN*35060-12 Note: Except...
Open the catalog to page 5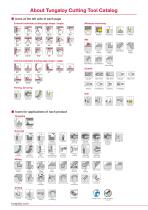
About Tungaloy Cutting Tool Catalog ■ Icons at the left side of each page Miniature machining External toolholder (cutting edge shape / angle) External Internal Grooving Threading Parting High feed Face Shoulder Slot milling milling milling milling Internal toolholder (cutting edge shape / angle) Chamfering Counterbore Finish face milling Parting, Grooving Radius Chamfering Slotting Threading External Internal 2-effective 4-effective Indexable Deep hole Reamer ■ Icons for applications of each product External External External grooving (full R) External Profiling grooving and turning (full R)...
Open the catalog to page 6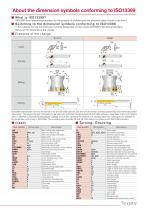
About the dimension symbols conforming to ISO13399 ■ W h at is ISO13 3 9 9? ISO13399 is an international standard for the purpose of standardizing the electronic data of tools in the world. ■ Switching to the dimension sy mbols confor ming to ISO13 3 9 9 In this catalog, we use the dimension symbols (properties) conforming to ISO13399 international standard. Below are the examples of the change. KAPR APMX Re (Effective flute length) R (Effective flute length) ISO13399 standardizes not only the format of 2D and 3D CAD data but also the tool dimension symbols (properties) and reference position...
Open the catalog to page 7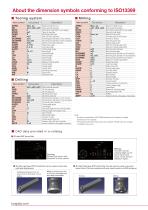
• Symbols unspecified in ISO13399 standard and Tungaloy’s original symbols are not included. • The symbols still under discussion are included. Please note any change or addition may occur. Shows the insert with standard corner radius. Milling: Includes actual cutting edge curve (CUT layer) and body cross section (NOCUT layer). • 3D data Light type (STP format file): Can be used to check tool path and interference. 3D data Detail type (STP format file): Can be used to create a new tool layout chart. (Can be combined with any insert model on a CAD software.) Turning: Equipped with an Milling:...
Open the catalog to page 8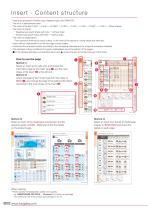
First choice for nishing. The sharp cutting edge and arc-shaped protrusion near the corner ensure excellent chip control. Unique geometry to provide better crater wear resistance and chip control during turning at light cutting depths. General-purpose chipbreaker with extensive chip control area. The protrusion in unique shape near the corner and large rake angle provide sharp cutting edge with low cutting force. Versatile geometry with optimized cutting edge design to provide superior chip control in wide range of applications. STAN DAR D C U TTIN G C OND ITION S Operation Precision finishing...
Open the catalog to page 10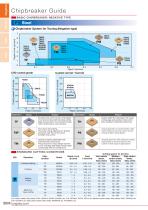
Chipbreaker Guide BASIC CHIPBREAKER: NEGATIVE TYPE Steel Chipbreaker System for Turning (Negative type) Q. Coated cermet / Cermet STANDARD CUTTING CONDITIONS Precision finishing Medium to heavy cutting steels, Alloy steels Cutting speed: Vc (m/min) carbon steels, Alloy steels High carbon steels, Alloy steels Low carbon steels, Alloy steels: S10C SCM415, SS400, SCr420H, etc. C10, 18CrMo4, E275A, 20Cr4, etc. Medium carbon steels, Alloy steels: S45C, SCM440, etc. C45, 42CrMo4, etc. High carbon steels, Alloy steels: SNCM439, etc. 41CrNiMo2, etc.
Open the catalog to page 12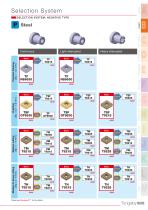
SELECTION SYSTEM: NEGATIVE TYPE Light interrupted Basic Fracture Chip control Basic Wear Crater wear Basic Fracture Basic Fracture Crater wear Basic Fracture Crater wear Chip control Basic Fracture Please see the page B*** for the details. Medium to heavy cutting [ ap = 3 ~ 6 mm ] Milling cutter Miniature tool Drilling tool Heavy interrupted User's Guide Tooling System
Open the catalog to page 13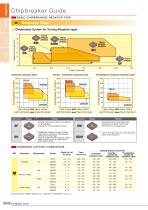
Chipbreaker Guide BASIC CHIPBREAKER: NEGATIVE TYPE Stainless Steel Chipbreaker System for Turning (Negative type) 7 6 5 4 3 Austenitic stainless steel Ferritic / martensite stainless steel Light cutting ■ Light interrupted - •Heavy cutting Heavy interrupted Precipitation hardened stainless steel 300 Light cutting < ► Heavy cutting Light interrupted 4 » Heavy interrupted Light cutting * ► Heavy cutting Light interrupted 4 * Heavy interrupted STANDARD CUTTING CONDITIONS ISO Operation Chipbreaker Grade Medium cutting Cutting speed: Vc (m/min) Austenitic stainless steel Ferritic / martensite stainless...
Open the catalog to page 14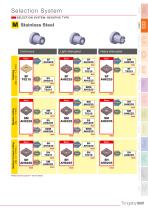
SELECTION SYSTEM: NEGATIVE TYPE Chip control Crater wear Basic Fracture Chip control Crater wear Basic Fracture Please see the page B*** for the details. Chip control Medium to heavy cutting [ ap = 2 ~ 6 mm ] Chip control Drilling tool Milling cutter Miniature tool Heavy interrupted User's Guide Tooling System Light interrupted Stainless Steel
Open the catalog to page 15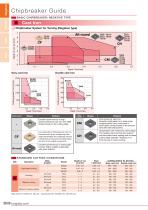
Chipbreaker Guide BASIC CHIPBREAKER: NEGATIVE TYPE Chipbreaker System for Turning (Negative type) Q_ Grey cast iron Ductile cast iron STANDARD CUTTING CONDITIONS Medium cutting Feed Cutting speed: Vc (m/min) f (mm/rev) Grey cast iron Ductile cast iron Grey cast iron: FC250, etc. 250, etc. Ductile cast iron: FCD450, etc. 450-10S, etc.
Open the catalog to page 16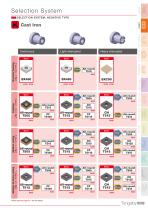
SELECTION SYSTEM: NEGATIVE TYPE Basic Wear Burr occurrence Burr occurrence Burr occurrence Burr occurrence Basic Wear Basic Wear Burr occurrence Basic Wear Please see the page B*** for the details. Burr occurrence Burr occurrence Basic Wear Burr occurrence Medium to heavy cutting [ ap = 3 ~ 6 mm ] Milling cutter Miniature tool Drilling tool Heavy interrupted User's Guide Tooling System Light interrupted Cast Iron
Open the catalog to page 17All Tungaloy EUROPE catalogs and technical brochures
 GENERAL CATALOG - VOL. 3 DRILLING
188 Pages
 GENERAL CATALOG - VOL. 2
404 Pages
Archived catalogs
 MY-T series
32 Pages
 New Procucts 2013
24 Pages
 Milling grade series T3130
6 Pages
 45° & 90° Milling cutter
12 Pages
 Stream Jet Bars
40 Pages
 Hybrid TAC MILL series
14 Pages
 boring tool-holder
26 Pages
 carbide drilling tool
8 Pages
 CBN cutting insert
16 Pages
 carbide cutting insert
20 Pages

- Chuck
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Storage cabinet
- Floor-mounted cabinet
- Metal milling cutter
- Clamping milling cutter
- Torque wrench
- Milling cutter with cylindrical shank
- Grade
- End mill
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Solid carbide milling cutter
- Indexable insert milling cutter