
- Catalogs
- TECNOMACCHINE
- Company presentation

Company presentation
Company presentation
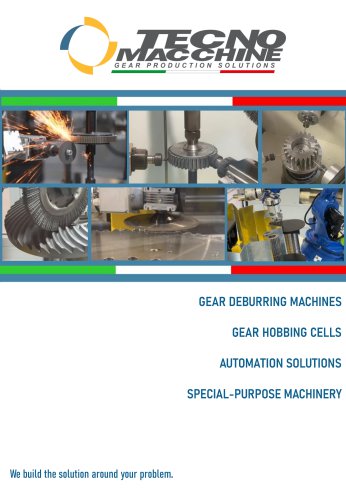
Tecnomacchine specializes in gear deburring and chamfering machines, offering solutions for various production scales and automation needs. Their machines are designed to enhance production efficiency and quality, with a focus on customization and customer satisfaction.
These processes are suitable for a wide range of applications, from small to large diameters and production series. Key advantages include repeatability, operator safety, low maintenance, and cost-effective tooling. Machines can be customized for flexibility or productivity.
With 20 years of experience, Tecnomacchine offers short delivery times due to stocked chassis and develops customized solutions. They provide comprehensive services from feasibility studies to assembly and inspection, and have expertise in industrial automation for integrated production lines.
Pre-machining with disk-cutters is offered as an alternative to manual filing. Standard chamfering uses abrasive wheels or end mills, followed by brushing to remove secondary burrs. Laser marking can be integrated for non-hardened materials. Tool adjustments can be manual or CNC-controlled.
Three tool adjustment options are available: handwheels for flexibility, manual adjustments with rotary counters, and CNC-controlled tools for efficiency. CNC-controlled tools reduce set-up time for recurring parts.
- Small Series Production: Machines like TM150 and TM1000 TBS offer solutions for small series with options for manual or pneumatic chucks and dust collectors.
- Medium-Sized Serial Production: Machines like TM250 and TM90 focus on reducing cycle time and set-up time with features like rotary tables and CNC control.
- Large Series Production: Machines like TM200-R3 and TM200-2C use rotary tables with multiple workstations to meet cycle time requirements and minimize downtime.
Automation solutions reduce operator presence and are suitable for medium to large series production. Systems like the Automated Basket Loader TM100 and Rotary Magazine Rotostore TM15 offer flexibility and extended autonomy.
Machines like TM T3 and TM T2 offer CNC-controlled drilling for gears, with features like automatic bit integrity checks and high throughput capabilities.
Tecnomacchine has international references and showcases successful results in chamfering and machining various gear types, demonstrating the effectiveness of their solutions.
Catalog excerpts
GEAR DEBURRING MACHINE GEAR HOBBING CELLS AUTOMATION SOLUTIO SPECIAL- PURPOSE MACHINER We build the solution around your.problem
Open the catalog to page 1
Mechanical Deburring Systems for Chamfering Toothed Parts •Mechanical chamfering Our deburring and chamfering solutions are suitable for almost any application: •From small to big diameters •From small to large series production We will define the most suitable machine type with you in order to satisfy your production requirements. Advantages of Mechanical Chamfering •Repeatability: constant quality of the machining result •Operators’ safety thanks to the closed structure of our machines machines which require little maintenance costs for chamfering tools equipment of the machine: from highly...
Open the catalog to page 2
Tools and Machining Process Pre-Machining via Disk-Cutter Especially the hobbing process of the geared parts generates burrs with significant dimensions. As an alternative to manual filing, Tecnomacchine offers a pre-machining process, during which the burr is cut off with a disk-cutter. Standard Chamfering It is possible to use both abrasive wheels (suitable for hardened and non-hardened material) as well as end mills (only suitable for non-hardened material). Depending on the chosen machine type, the tools can be adjusted manually or can be CNCcontrolled. The pressure of the tool is adjustable...
Open the catalog to page 3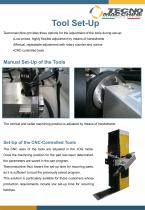
Tool Set-Up Tecnomacchine provides three options for the adjustment of the tools during set-up: •Low-priced, highly flexible adjustment by means of handwheels •Manual, repeatable adjustment with rotary counter and nonius •CNC-controlled tools Manual Set-Up of the Tools The vertical and radial machining position is adjusted by means of handwheels. Set-Up of the CNC-Controlled Tools The CNC axes of the tools are adjusted in the JOG mode. Once the machining position for the part has been determined, the parameters are saved in the part program. Tecnomacchine thus lowers the set-up time for recurring...
Open the catalog to page 4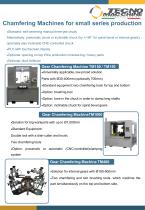
Chamfering Machines for small series production •Standard: self-centering manual three-jaw chuck Alternatively: pneumatic chuck or inclinable chuck (by +/-90° for spiral bevel or internal gears), optionally also inclinable CNC-controlled chuck •PLC with touchscreen display opening on top if the production includes big / heavy parts dust collector Gear Chamfering Machine TM150 / TM150 big •Universally applicable, low-priced solution Parts with Ø30-400mm (optionally 700mm) •Standard equipment: two chamfering tools for top and bottom brushing tool bore in the chuck in order to clamp long shafts...
Open the catalog to page 5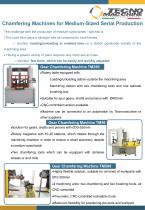
Chamfering Machines for Medium-Sized Serial Production The challenge with the production of medium-sized series / batches is: •The cycle time plays a stronger role as compared to small series. → solution: loading/unloading in masked time on a station positioned outside of the machining area • Having a greater variety of parts requires very short set-up times → solution: few tools, which can be easily and quickly adjusted Gear Chamfering Machine TM250 •Rotary table equipped with: Loading/unloading station outside the machining area Machining station with two chamfering tools and one optional brushing...
Open the catalog to page 6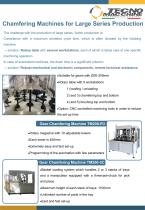
Chamfering Machines for Large Series Production The challenge with the production of large series / batch production is: Compliance with a maximum admitted cycle time, which is often dictated by the hobbing machine → solution: Rotary table with several workstations, each of which is takes care of one specific machining operation In case of automated machines, the down time is a significant criterion → solution: Robust mechanical and electronic components, remote technical assistance •Suitable for •Rotary table with 5 workstations 1) loading / unloading 2) and 3) chamfering top and bottom 4) and...
Open the catalog to page 7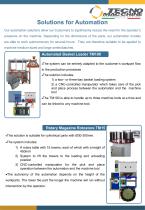
Solutions for Automation Our automation solutions allow our Customers to significantly reduce the need for the operator’s presence on the machine. Depending on the dimensions of the parts, our automation models are able to work autonomously for several hours. They are therefore suitable to be applied to machine medium-sized and large series/batches. Automated Basket Loader TM100 •The system can be entirely adapted to the customer’s workpart flow in the production processes •The solution includes: 1) a two- or three-bay basket loading system 2) a CNC-controlled manipulator which takes care of...
Open the catalog to page 8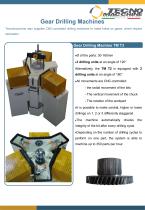
Gear Drilling Machines Tecnomacchine also supplies CNC-controlled drilling machines to make holes on gears, which require lubrication. Gear Drilling Machine TM T3 •Ø drilling units at an angle of 120° Alternatively, the TM T2 is equipped with 2 drilling units at an angle of 180° •All movements are CNC-controlled: - the radial movement of the bits - The vertical movement of the chuck - The rotation of the workpart is possible to make central, higher or lower drillings on 1, 2 or 3 differently staggered •The integrity of the bit after every drilling cycle. •Depending on the number of drilling cycles...
Open the catalog to page 9
mmncHO REGGIANA Bonfiglioli < CARRARO GROUP industries BOgMAt tensili unO\S Leons iu Pdweriraiw Solutions CATTINI & FIGLIO Shift gear, together VARVEL BONDIOLI
Open the catalog to page 10
International References Professional Agrotechnics KEEP THE WORLD IN MOTION 0/TROJNA IN tizaTeC Gallwieland ANTftlESSlECHNIK Solar Turbines ~ttaezklEO mayr & MACHINING Dtvtaro* or HAmiKK AmmociArra Di$U OTOMOTIV SANAYi VF Ti( PREMIUM GEARS
Open the catalog to page 11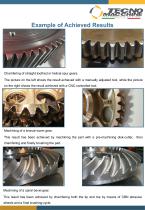
Example of Achieved Results Chamfering of straight-toothed or helical spur gears. The picture on the left shows the result achieved with a manually adjusted tool, while the picture on the right shows the result achieved with a CNC-controlled tool. Machining of a bronze worm gear. This result has been achieved by machining the part with a pre-machining disk-cutter, then chamfering and finally brushing the part. Machining of a spiral bevel gear. This result has been achieved by chamfering both the tip and toe by means of CBN abrasive wheels and a final brushing cycle.
Open the catalog to page 12- CNC drilling machine
- Brush deburring machine
- Automatic deburring machine
- Finishing deburring machine
- CNC deburring machine
- Storage paternoster
- Disc deburring machine
- Brushing deburring machine
- Chamfering deburring machine
- Stationary deburring machine
- Multi-station deburring machine
- Manual deburring machine
- 3-axis drilling machine
- Multi-spindle drilling machine
- Pre-deburring deburring machine
- 3-spindle drilling machine
- Manually-operated deburring machine
- Gear teeth deburring machine