
- Catalogs
- ROL d.o.o.
- REV Tool - Broaching
REV Tool - Broaching
REV Tool - Broaching
The document outlines detailed specifications for various tool and component codes, including measurements such as length (L1, L2, L3), diameter (D1, D2, D3), and weight. It specifies compatible tools and resharpeners for each code, ensuring proper usage and compatibility.
Although primarily focused on specifications, the document suggests procedures for selecting appropriate tools based on measurements and compatibility with resharpeners and screwdrivers. It also lists threaded holes and hexagonal wrench sizes for assembly and maintenance.
The document adheres to measurement standards, using both metric (mm) and imperial (inches) units, ensuring compatibility with standard tool sizes and resharpeners. It follows a standardized coding system for easy part identification.
Recommendations are implicit, advising users to select tools and resharpeners that match specified measurements for optimal performance. It emphasizes using specified tools and sizes for each component to ensure proper fit and function.
Tables provide a comprehensive list of tool codes with corresponding measurements and compatible tools. Key data includes tool codes (e.g., UT-02-25, IN-02 P9), measurements in mm and inches, compatible tools and resharpeners (e.g., UT-02, RF-0), and weight in grams.
Critical information includes the minimum hole size required for each tool, the weight of each component, and the specific screwdriver and clamping screw needed for assembly. It also highlights the importance of using the correct TORX and TCEI screws as per specified codes and paying attention to the tool carrier housing hole shape and diameter for proper assembly.
Catalog excerpts
COMPANY PROFILE Company, F.P. Officina Meccanica (now REV s.r.l.) , was founded in 1998 based on Mr. Paolo Franchini's 18 years of experience in the mechanics industry. For many years, the Company carried out slotting and broaching activities for third-parties, working in the hydraulic, automotive, biomedical, speed reducers, gear construction and earth moving machinery industries, etc., ... Over time, in addition to slotting and broaching, the Company began CNC lathing and milling mechanical parts, which also often involved producing internal keyways, and six-spline PTOs. Not only did it require...
Open the catalog to page 2
INDEX I he REV Broaching Tool can be used for processes requiring straight cuts, such as broaching tab or key housings, PTOs and internal gears, directly on CNC lathes, machining centres or milling machines, considerably faster and with remarkable precision. In addition to offering the significant advantage of not having to pick up the workpiece for broaching or slotting and set it up on another dedicated machine, the tool also makes sure the broaching process is carried out correctly, at the same time as the other processes. Used on slotting or shaping machines, the REV tool represents an excellent...
Open the catalog to page 3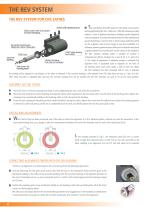
The main feature of the REV system for CNC lathes is the eccentric bushing patented by REV S.R.L. (Patent no. 1.394.481) allowing any lathe without a Y-axis to perform broaching or slotting in perfect alignment with the workpiece. It is made with tool steel which is then hardened and ground. Broaching is a process that is almost always perfectly centred on the workpiece, with an error margin of very few hundredths of a millimetre, however, symmetry errors often occur in relation to mechanical coupling between the mounted tool and the centre of the workpiece. The REV eccentric bushing makes it...
Open the catalog to page 4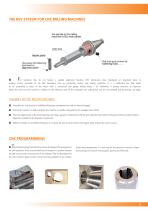
THE REV SYSTEM FOR CNC MILLING MACHINES ■ For machines that do not feature a spindle alignment function, REV technicians have developed an alignment plate to achieve correct assembly of the REV Broaching Tool on machining centres and milling machines. It is a calibrated bar that needs to be assembled in place of the insert, with a centesimal dial gauge sliding along it (or millesimal, if greater precision is required). When the tool has been centred in relation to the reference axes of the workpiece, the cutting tool can be re-assembled and processing can begin. ASSEMBLY ON CNC MILLING MACHINES...
Open the catalog to page 5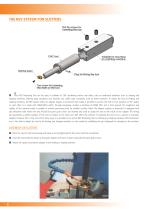
Slotting insert Plug for timing the tool Torx screw for fastening the inserr on the tool ■ The REV Broaching Tool can be used, in addition to CNC machining centres and lathes, also on traditional machines such as slotting and shaping machines, offering great sturdiness and versatile use, unlike tools commonly used on these machines. To clamp the tool to slotting and shaping machines, the REV system offers an adapter (square or prismatic) that makes it possible to process the hole in four positions at 90° angles to each other. It is made with 39NiCrM03 which, through tempering, reaches a hardness...
Open the catalog to page 6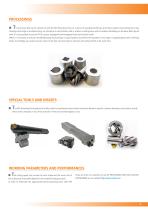
■ I he processes that can be carried out with the REV Broaching Tool are, in terms of standard machining, all of those relative to broaching tab or key housings with single or multiple timing, on cylindrical or conical holes, with or without a relief groove, with or without chamfering on the base. With special tools it is also possible to execute PTOs, square, pentagonal and hexagonal holes and involute teeth. When it is necessary to execute considerably large key housings, it is good practice to perform the operation in two steps: a roughing phase and a finishing phase. Accordingly, you avoid...
Open the catalog to page 7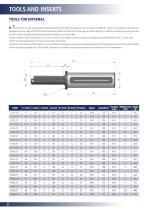
■ The REV tools are made with quenched and tempered tool steel. The section that houses the insert is hardened to 58/60 HRC, making it very resistant to compression and guaranteeing the tool a long service life. The REV Broaching Tool feature 4 mm holes for the forced supply of coolant liquid which, in addition to lubricating and cooling the insert, are used to extract the chips, produced through broaching or slotting, out of the blind hole. The tool is available in two socket diameters (25 and 32). Two tool lines are available for each socket diameter: standard and long (identified by the suffix"...
Open the catalog to page 8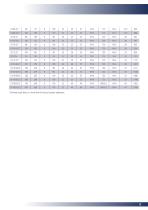
*0n these tools there is a 4mm hole for forced coolant adduction.
Open the catalog to page 9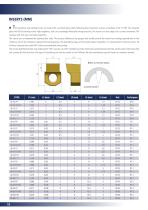
■ I he broaching and slotting inserts are made with a sintered alloy which, following heat treatment, reaches a hardness of 70-71 HRC. This material gives the REV broaching inserts high toughness, and can accordingly withstand strong pressures. The inserts are also subject to a surface treatment, TiN coating, with anti wear and seize properties. The inserts are re-sharpened by tapering their sides. This process eliminates any gouges that would prevent the insert from cutting perpendicular to the reference axis of the workpiece during the broaching phase. The protruding shape of the inserts makes...
Open the catalog to page 10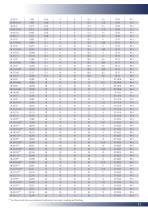
**For these insert sizes we recommend machining in two steps: roughing and finishing.
Open the catalog to page 11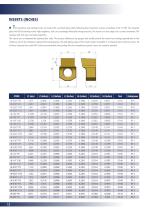
■ I he broaching and slotting inserts are made with a sintered alloy which, following heat treatment, reaches a hardness of 70-71 HRC. This material gives the REV broaching inserts high toughness, and can accordingly withstand strong pressures. The inserts are also subject to a surface treatment, TiN coating, with anti wear and seize properties. The inserts are re-sharpened by tapering their sides. This process eliminates any gouges that would prevent the insert from cutting perpendicular to the reference axis of the workpiece during the broaching phase. The protruding shape of the inserts makes...
Open the catalog to page 12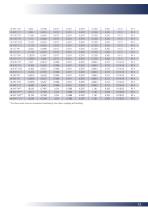
**For these insert sizes we recommend machining in two steps: roughing and finishing.
Open the catalog to page 13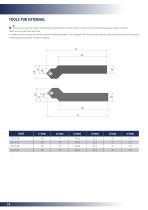
These tools are made with tool steel. In addition to the two types of tools for external machining available in the catalogue, the REV production facility is able to build special tools for external machining based on specific customer demands.
Open the catalog to page 14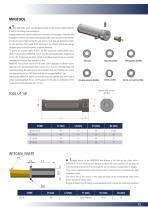
MINITOOL ■ I he MINITOOL series was developed based on the need to satisfy demands linked to machining small workpieces. Integral inserts were used to satisfy these demands, as these types of inserts make it possible to achieve extremely small cutting profiles, with very diverse geometries. In order to ensure high tool rigidity and achieve tools that are absolutely perfect for the operation that needs to be performed, the integral inserts are always designed ad hoc based on specific customer demands. To ensure the prompt supply of tools, the REV production facility always has a stock of semi-finished...
Open the catalog to page 15All ROL d.o.o. catalogs and technical brochures
 Alpa metrology
325 Pages
 Kinex measuring instruments
92 Pages
 Cutting Promo
2 Pages
 SAU Catalog
1236 Pages
 Schüssler Clamping Technology
172 Pages
 Mimatic
181 Pages
 Helion
282 Pages
 PhantomEU
690 Pages
 Schüssler Clamping Technology
172 Pages
 EMAC Clamping Technology
411 Pages
 Chia-Mo Clamping Technology
252 Pages
 Mack Werkzeuge Catalog
340 Pages
 FATPOL TOOLS
276 Pages
 Mini Solid Carbide Tools
56 Pages
 NUI Drilling Catalog
214 Pages
 Integi catalog
90 Pages
 PROMO Catalog
20 Pages
 ROL catalog
188 Pages
- Milling tool
- Chuck
- Solid milling cutter
- Drilling tool
- Milling tool with replaceable insert
- End mill
- Face milling cutter
- Multi-purpose drilling tool
- Cutting milling cutter
- Helix angle milling cutter
- Shoulder milling cutter
- Tungsten carbide drill bit
- Milling chuck
- Slot milling tool
- Cutting edge milling cutter
- 2-flute milling cutter
- Collet chuck
- Milling tool holder
- CNC machine milling cutter
- High-speed milling cutter