
- Catalogs
- Resodyn Acoustic Mixers, Inc.
- LabRAM II H
- Company
- Products
- Catalogs
- News & Trends
- Exhibitions
LabRAM II H
LabRAM II H
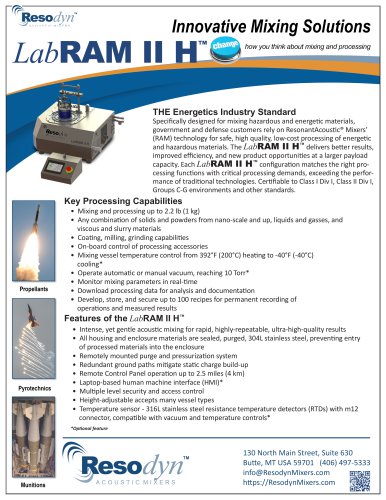
The document outlines the capabilities and specifications of the LabRAM II H™, a ResonantAcoustic® Mixer designed for safe and efficient processing of hazardous and energetic materials. It is particularly used by government and defense sectors for its high-quality, low-cost processing capabilities.
Key Features and Capabilities
- Mixing and processing capacity of up to 2.2 lb (1 kg) for various materials including solids, powders, liquids, and gases.
- Capabilities include coating, milling, and grinding.
- Temperature control ranging from 392°F (200°C) to -40°F (-40°C).
- Automatic or manual vacuum operation reaching 10 Torr.
- Real-time monitoring and data logging for analysis and documentation.
- Storage for up to 100 programmable mix recipes.
- Sealed, purged 304L stainless steel housing to prevent material entry.
- Remote operation capability up to 2.5 miles (4 km) with a laptop-based HMI.
- Multiple security and access control levels.
Specifications
- Maximum payload capacity: 2.2 lb (1 kg).
- Human Machine Interface: Full Color Touch Screen.
- Operating System: Proprietary On-Board.
- Max Vessel Acceleration: 100g at approximately 60 Hz.
- Unit Dimensions: 27″ H x 32″ W x 30″ D (68.6 x 81.3 x 76.2 cm).
- Unit Weight: 310 lb (141 kg).
- Certifications: CE, UL, ATEX, IECEx, Class I Div 1, Class II Div 1, CSA, IP65.
- Required Voltage: 100-120 / 200-240 VAC (50-60 Hz).
Global Impact and Applications
Since its introduction in 2007, RAM technology has been adopted by Fortune 500 companies and production facilities in 38 countries. It offers 10-100x faster processing, reliable repeatability, and direct scalability from laboratory to production without increased processing time. The RAM product line includes various models with capacities ranging from 2.2 lb to 920 lb, all utilizing low-frequency acoustic mixing for intense, low-shear results.
Catalog excerpts

ACOUSTIC MIXERS Innovative Mixing SolutionsTHE Energetics Industry Standard Specifically designed for mixing hazardous and energetic materials, government and defense customers rely on ResonantAcoustic® Mixers' (RAM) technology for safe, high quality, low-cost processing of energetic and hazardous materials. The LabRAM II H delivers better results, improved efficiency, and new product opportunities at a larger payload capacity. Each LabRAM II H configuration matches the right processing functions with critical processing demands, exceeding the performance of traditional technologies. Certifiable to Class I Div I, Class II Div I, Groups C-G environments and other standards. • Any combination of solids and powders from nano-scale and up, liquids and gasses, and viscous and slurry materials • Coating, milling, grinding capabilities • On-board control of processing accessories • Mixing vessel temperature control from 392°F (200°C) heating to -40°F (-40°C) cooling* • Operate automatic or manual vacuum, reaching 10 Torr* • Monitor mixing parameters in real-time • Download processing data for analysis and documentation • Develop, store, and secure up to 100 recipes for permanent recording of operations and measured results • Intense, yet gentle acoustic mixing for rapid, highly-repeatable, ultra-high-quality results • All housing and enclosure materials are sealed, purged, 304L stainless steel, preventing entry of processed materials into the enclosure • Remotely mounted purge and pressurization system • Redundant ground paths mitigate static charge build-up • Remote Control Panel operation up to 2.5 miles (4 km) • Laptop-based human machine interface (HMI)* • Multiple level security and access control Height-adjustable accepts many vessel types Temperature sensor - 316L stainless steel resistance temperature detectors (RTDs) with m12 connector, compatible with vacuum and temperature controls* 130 North Main Street, Suite 630 Butte, MT USA 59701 (406) 497-5333 [email protected] HSSiH https://ResodynMi
Open the catalog to page 1
Innovative Mixing Solutions Since its introduction to the marketplace in 2007, ResonantAcoustic® Mixers' (RAM) technology has become the choice for many commercial mixing and processing applications. RAM's unique combination of features and performance has proven successful at Fortune 500 laboratories and production facilities in 38 countries across a broad range of industries. ResonantAcoustic® Mixing (RAM) Product Line Features LabRAM II H™performance extends across the RAM product line, enabling new product development and break-through results not possible with traditional mixing methods....
Open the catalog to page 2All Resodyn Acoustic Mixers, Inc. catalogs and technical brochures
 OmniRAM H
2 Pages
 RAM 5 H™
2 Pages
 OmniRAM Pharma
2 Pages
 Ceramics
10 Pages
 PharmaRAM Compounding
1 Page
 Nano Suspension
1 Page
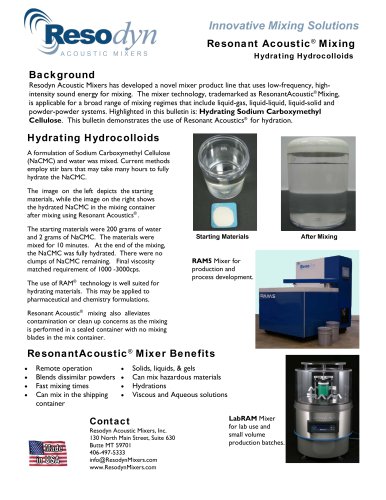 Hydrating Hydrocolloids
1 Page
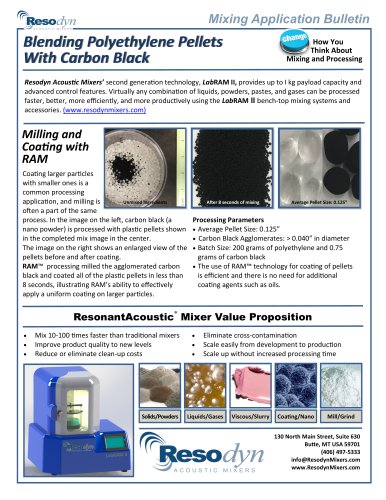 Milling and Coating with RAM
2 Pages
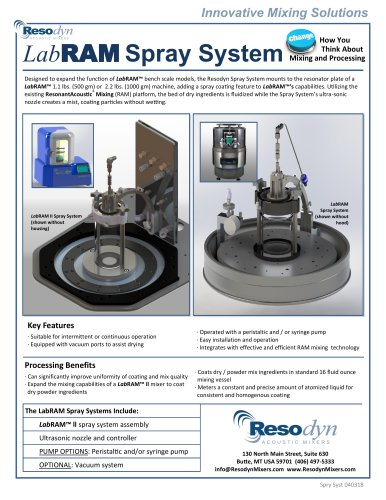 Spray System
2 Pages
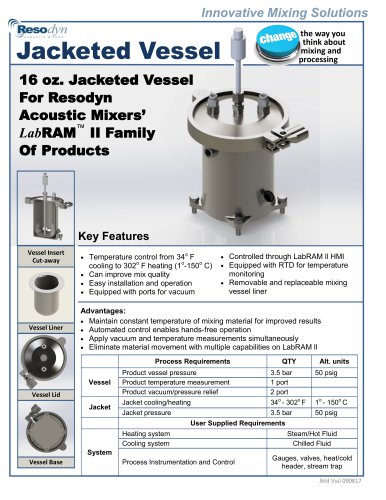 16oz Jacketed Vessel
2 Pages
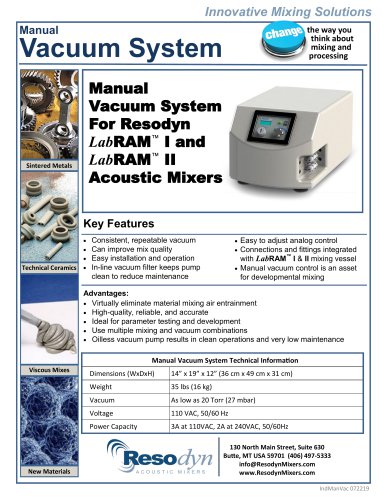 Manual Vacuum System
2 Pages
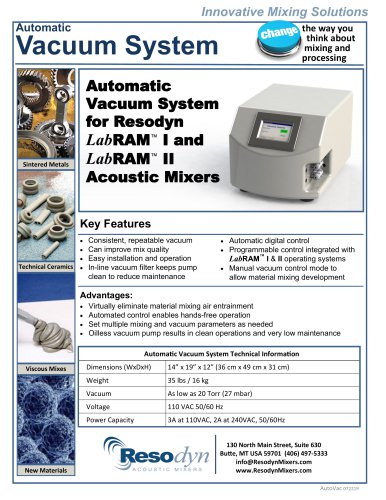 Automatic Vacuum System
2 Pages
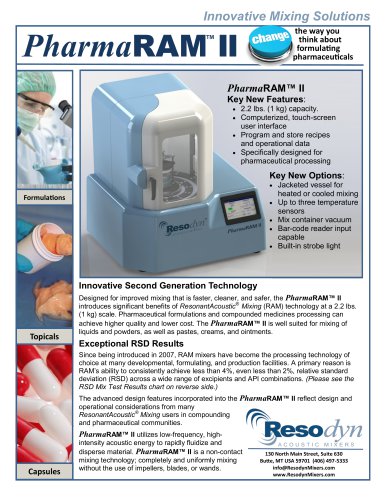 PharmaRAM II
2 Pages
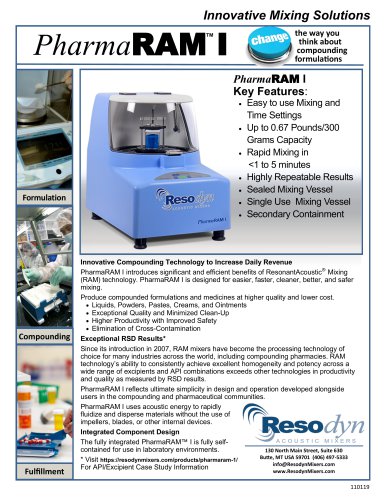 PharmaRAM I
2 Pages
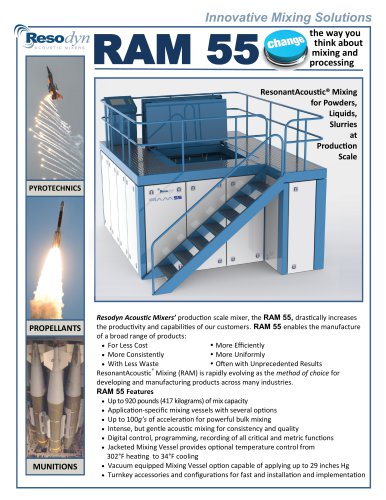 RAM 55
2 Pages
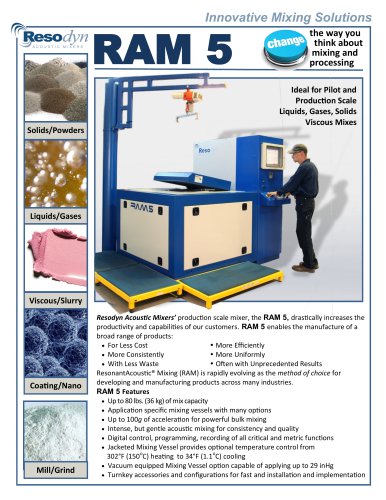 RAM 5
2 Pages
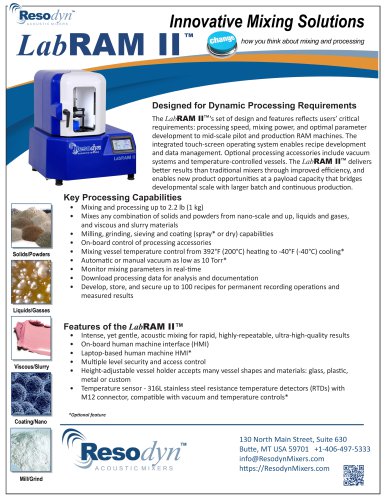 OmniRAM ™
2 Pages
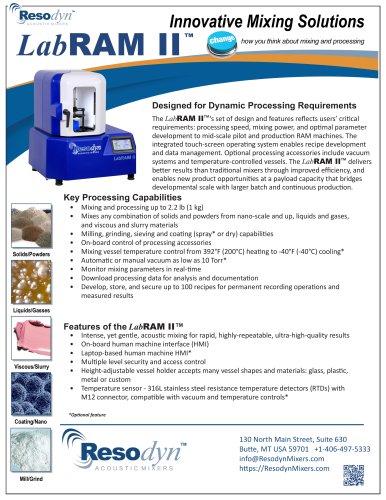 LabRAM II™
2 Pages
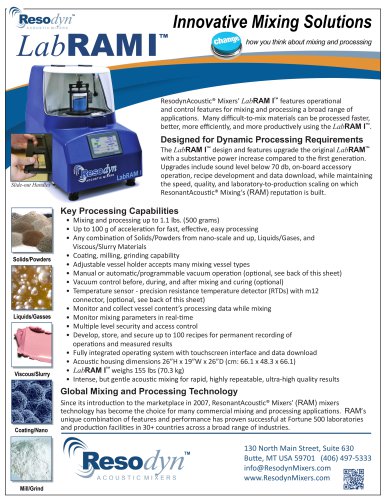 LabRAM I™
2 Pages
- Resodyn batch mixer
- Liquid homogenizer
- Resodyn vertical mixer
- Resodyn mixer for the chemical industry
- Resodyn stainless steel mixer
- Laboratory shaker
- In-line mixer
- Resodyn solid mixer
- Resodyn solids/liquids mixer
- Resodyn powder mixer
- Resodyn mixer for the pharmaceutical industry
- Digital laboratory stirrer
- Agitator for the cosmetics industry
- Bench-top laboratory shaker
- Solid kneader
- Compact homogenizer
- High-speed blender
- Vacuum blender
- Resodyn laboratory mixer
- Explosion-proof agitator