
- Company
- Products
- Catalogs
- News & Trends
- Exhibitions
UHT
UHT
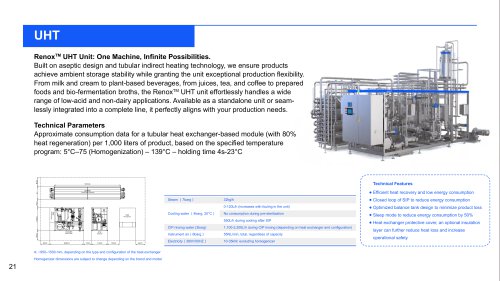
- Efficient heat recovery and low energy consumption through a closed loop of SIP, optimized balance tank design, and sleep mode reducing energy consumption by 50%.
- Optional heat exchanger protective cover and insulation layer to reduce heat loss and enhance operational safety.
The RenoxTM UHT Unit is designed with aseptic design and tubular indirect heating technology, providing ambient storage stability and production flexibility. It is suitable for a wide range of applications including milk, cream, plant-based beverages, juices, tea, coffee, prepared foods, and bio-fermentation broths. It can be used as a standalone unit or integrated into a complete production line.
Technical Parameters- Consumption data for a tubular heat exchanger-based module with 80% heat regeneration per 1,000 liters of product, based on a temperature program of 5°C–75°C (Homogenization) – 139°C – holding time 4s-23°C.
- Dimensions and consumption details:
- Heat exchanger dimensions: ~950–1500 mm, depending on type and configuration.
- Steam consumption: 32kg/h at 7barg.
- Cooling water: 0-120L/h at 4barg, 20°C, increasing with fouling.
- CIP rinsing water: 1,100-2,200L/h during CIP rinsing, depending on configuration.
- Instrument air: 55NL/min, total.
- Electricity: 10-35kW, excluding homogenizer.
Catalog excerpts
UHT RenoxTM UHT Unit: One Machine, Infinite Possibilities. Built on aseptic design and tubular indirect heating technology, we ensure products achieve ambient storage stability while granting the unit exceptional production flexibility. From milk and cream to plant-based beverages, from juices, tea, and coffee to prepared foods and bio-fermentation broths, the RenoxTM UHT unit effortlessly handles a wide range of low-acid and non-dairy applications. Available as a standalone unit or seamlessly integrated into a complete line, it perfectly aligns with your production needs. Technical Parameters Approximate consumption data for a tubular heat exchanger-based module (with 80% heat regeneration) per 1,000 liters of product, based on the specified temperature program: 5°C–75 (Homogenization) – 139°C – holding time 4s-23°C Technical Features Efficient heat recovery and low energy consumption Tubular heat exchanger Control panel Closed loop of SIP to reduce energy consumption 0-120L/h (increases with fouling in the unit) Optimized balance tank design to minimize product loss No consumption during pre-sterilization Sleep mode to reduce energy consumption by 50% 550L/h during cooling after SIP Heat exchanger protective cover, an optional insulation Feed module A: ~950–1500 mm, depending on the type and configuration of the heat exchanger Homogenizer dimensions are subject to change depending on the brand and model 1,100-2,200L/h during CIP rinsing (depending on heat exchanger and configuration) 55NL/min, total, regardless of capacity
Open the catalog to page 1All Renox Flow catalogs and technical brochures
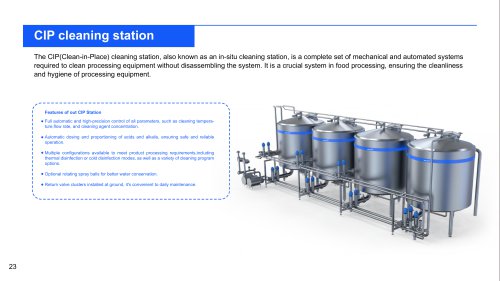 CIP Cleaning station
1 Page
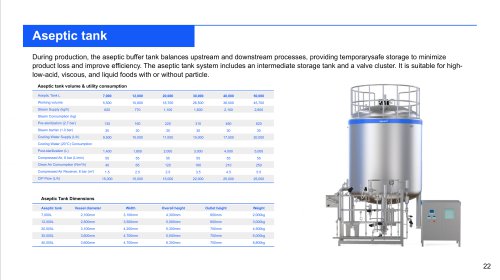 Aspetic tank
1 Page
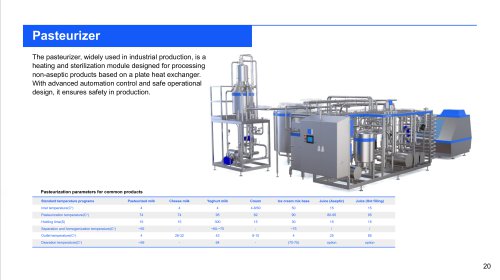 Pasteurizer
1 Page
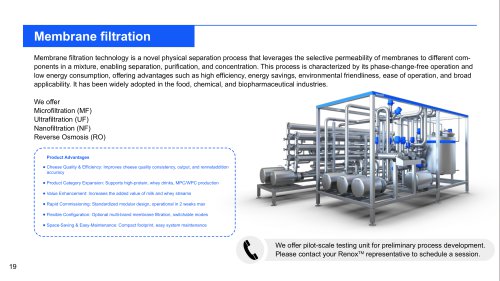 Membrane filtration
1 Page
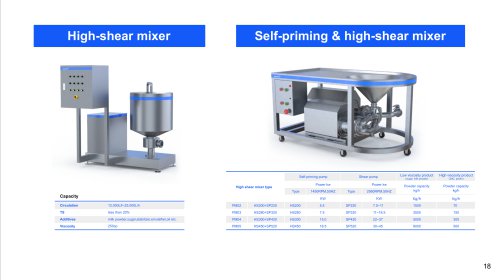 High shear mixer
1 Page
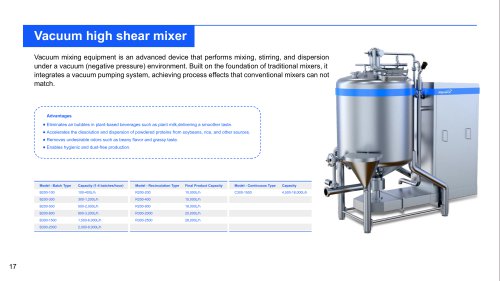 High shear mixer
1 Page
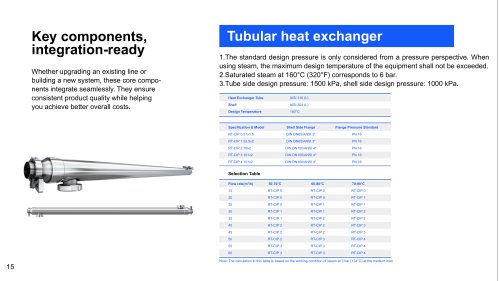 Tubular heat exchanger
1 Page
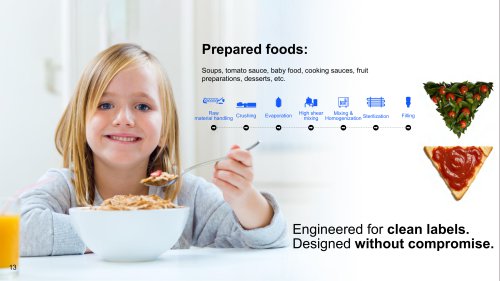 prepared foods
1 Page
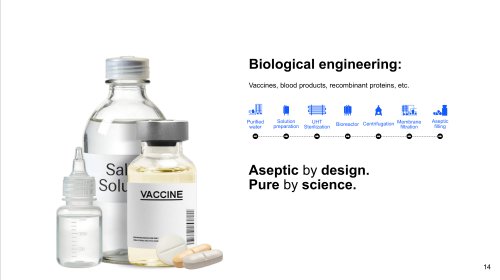 Biological Engineering
1 Page
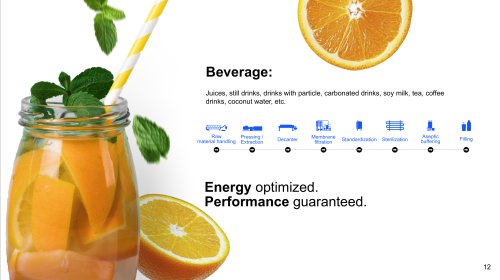 Beverage
1 Page
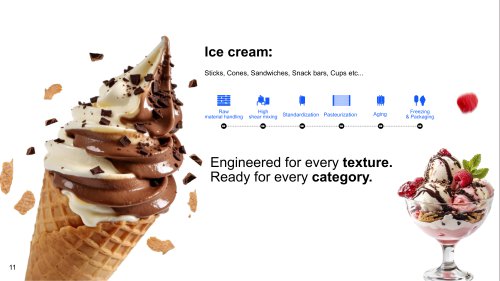 Ice Cream
1 Page
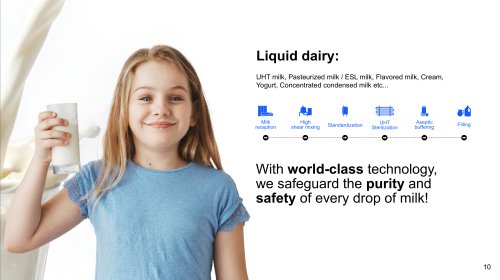 Liquid Dairy
1 Page
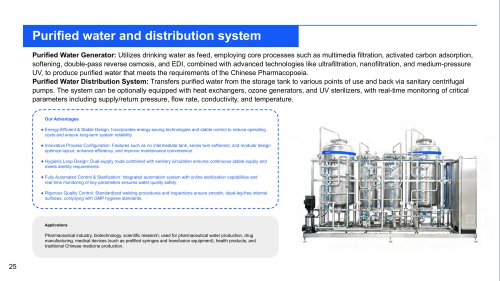
- Dynamic agitator
- Batch agitator
- Automatic cleaning system
- Liquid homogenizer
- Water cleaning system
- Agitator for the food industry
- Automated production line
- In-line mixer
- Solid mixer
- Solid/liquid agitator
- Powder kneader
- Blender for the pharmaceutical industry
- Real-time monitoring module
- Agitator for the cosmetics industry
- Water purification unit
- High-speed blender
- Vacuum blender
- Turbine homogenizer
- Condition monitoring module