
- Catalogs
- Renox Flow
- Membrane filtration
- Company
- Products
- Catalogs
- News & Trends
- Exhibitions
Membrane filtration
Membrane filtration
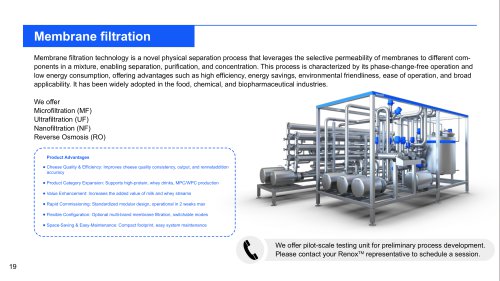
Membrane filtration is a cutting-edge physical separation process that utilizes the selective permeability of membranes to separate, purify, and concentrate components in a mixture. This technology operates without phase changes and is known for its low energy consumption, making it efficient, environmentally friendly, and easy to operate. It is widely used in industries such as food, chemical, and biopharmaceuticals.
- Microfiltration (MF)
- Ultrafiltration (UF)
- Nanofiltration (NF)
- Reverse Osmosis (RO)
- Cheese Quality & Efficiency: Enhances consistency, output, and rennet addition accuracy in cheese production.
- Product Category Expansion: Facilitates the production of high-protein drinks, whey drinks, and milk protein concentrates (MPC/WPC).
- Value Enhancement: Increases the added value of milk and whey streams.
- Rapid Commissioning: Features a standardized modular design that can be operational within two weeks.
- Flexible Configuration: Offers optional multi-brand membrane filtration with switchable modes.
- Space-Saving & Easy Maintenance: Designed with a compact footprint and easy system maintenance.
A pilot-scale testing unit is available for preliminary process development. Contact your RenoxTM representative to schedule a session.
Catalog excerpts
Membrane filtration technology is a novel physical separation process that leverages the selective permeability of membranes to different components in a mixture, enabling separation, purification, and concentration. This process is characterized by its phase-change-free operation and low energy consumption, offering advantages such as high efficiency, energy savings, environmental friendliness, ease of operation, and broad applicability. It has been widely adopted in the food, chemical, and biopharmaceutical industries. [ • Cheese Quality & Efficiency: Improves cheese quality consistency, output, and rennetaddition j • Product Category Expansion: Supports high-protein, whey drinks, MPC/WPC production l • Value Enhancement: Increases the added value of milk and whey streams , • Rapid Commissioning: Standardized modular design, operational in 2 weeks max 1 • Flexible Configuration: Optional multi-brand membrane filtration, switchable modes I • Space-Saving & Easy-Maintenance: Compact footprint, easy system maintenance We offer pilot-scale testing unit for preliminary process development. Please contact your Renox™ representative to schedule a session.
Open the catalog to page 1All Renox Flow catalogs and technical brochures
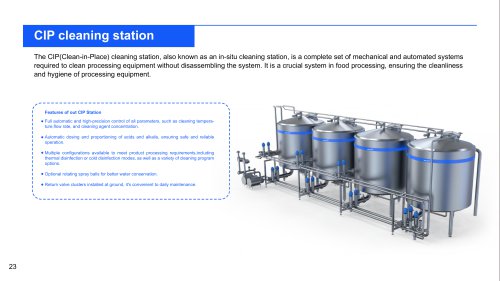 CIP Cleaning station
1 Page
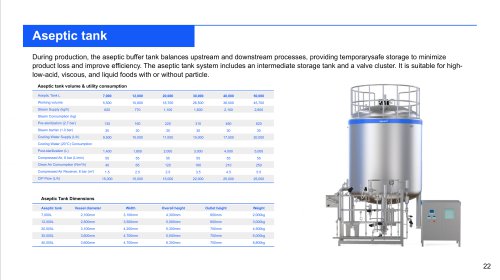 Aspetic tank
1 Page
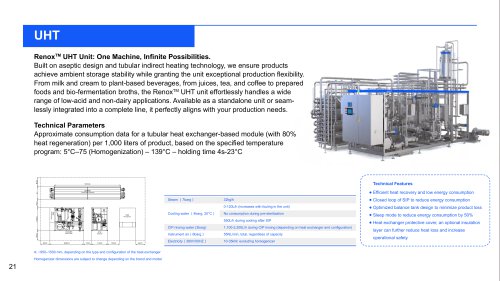 UHT
1 Page
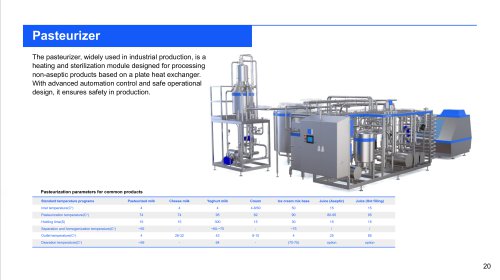 Pasteurizer
1 Page
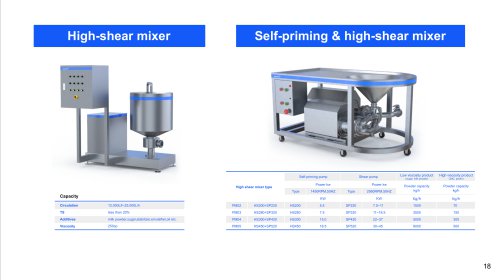 High shear mixer
1 Page
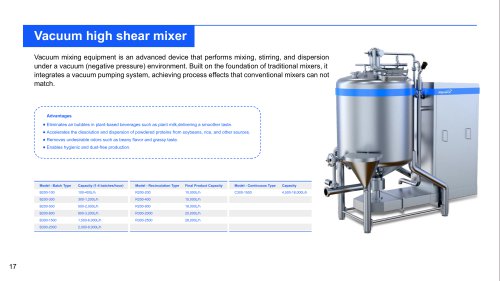 High shear mixer
1 Page
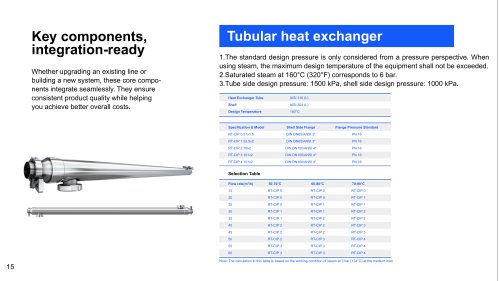 Tubular heat exchanger
1 Page
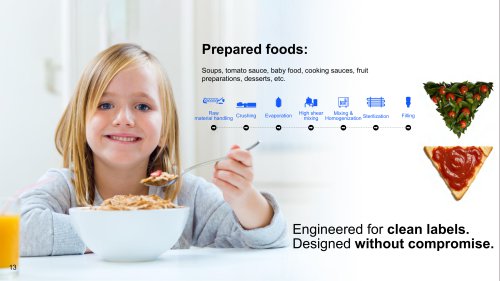 prepared foods
1 Page
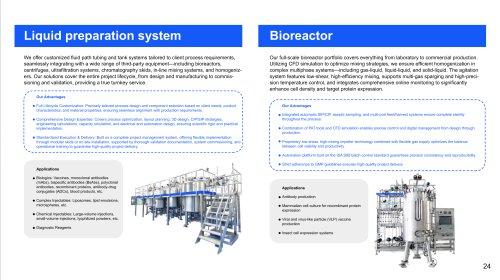
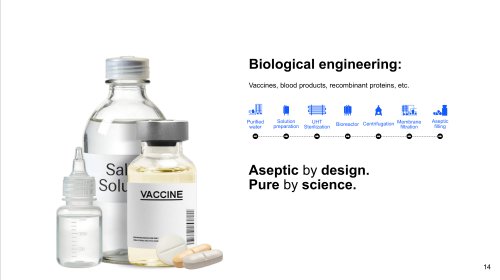 Biological Engineering
1 Page
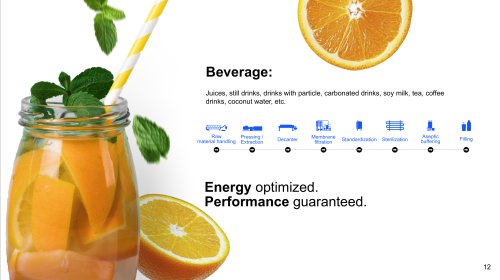 Beverage
1 Page
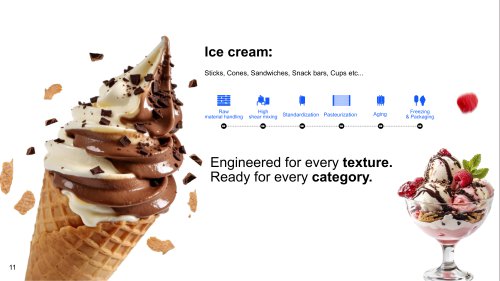 Ice Cream
1 Page
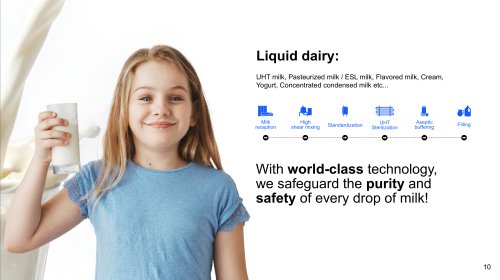 Liquid Dairy
1 Page
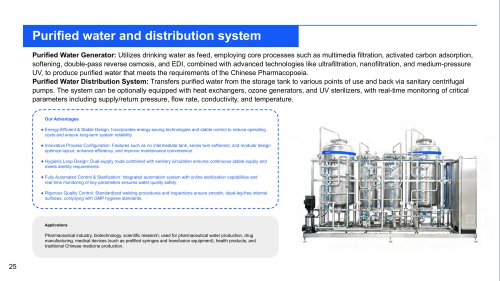
- Dynamic agitator
- Batch agitator
- Automatic cleaning system
- Making machine
- Liquid homogenizer
- Water cleaning system
- Agitator for the food industry
- Automated production line
- In-line mixer
- Solid mixer
- Solid/liquid agitator
- Powder kneader
- Blender for the pharmaceutical industry
- Real-time monitoring module
- Agitator for the cosmetics industry
- Water purification unit
- High-speed blender
- Vacuum blender
- Turbine homogenizer
- Condition monitoring module