
- Catalogs
- NACHI America
- AG Power Drills Series

- Products
- Catalogs
- News & Trends
- Exhibitions
AG Power Drills Series

AG Power Drills Series
Overview
This document details the AG Power series of high-speed steel (HSS) drills, designed for high-efficiency, fast-feed machining. It covers three main product lines—regular (AGPSD), semi-long (AGPSLSD), and long drills (AGPLSD)—each tailored for specific hole depths and machining needs.
Product Lines and Specifications
- AGPSD (Regular Size Drills): Suitable for hole depths up to 5×D, diameters 1.0–13.0 mm. Features high rigidity and a non-step flute design for efficient chip evacuation.
- AGPSLSD (Semi-long Drills): Designed for hole depths 5×D to 10×D, diameters 1.0–13.0 mm. Supports stable non-step drilling up to 7×D.
- AGPLSD (Long Drills): For deep holes up to 20×D, diameters 1.0–20.0 mm. Optimized for wear resistance and chip evacuation in deep hole drilling.
Key Features and Benefits
- AG Coating: Advanced cross-sectional coating enhances wear resistance, extending tool life significantly.
- Non-step Flute Design: Maintains drill rigidity while improving chip discharge, reducing cutting resistance and increasing machining stability.
- Cutting Performance: Lower thrust and torque compared to conventional drills enable faster feed rates and shorter machining times.
- Material Compatibility: Suitable for carbon steels, alloy steels, pre-hardened steels (25–40 HRC), some stainless steels, and titanium alloys. Not recommended for materials above 50 HRC or certain stainless steels (e.g., SUS304, SUS316).
Cutting Conditions and Machining Parameters
Recommended cutting speeds, spindle speeds, feed speeds, and feed per revolution vary by drill size and material. Examples include:
- AGPSD 3.0 mm: 30 m/min cutting speed, 3,180 rpm, 330 mm/min feed, 0.1 mm/rev feed.
- AGPSD 6.0 mm: 24 m/min, 1,272 rpm, 230 mm/min feed, 0.18 mm/rev.
- AGPSLSD 3.0 mm: 24 m/min, 2,500 rpm, 200 mm/min feed, 0.08 mm/rev.
- AGPLSD 6.0 mm: 18–30 m/min, 955–1,590 rpm, 143–160 mm/min feed, 0.1–0.15 mm/rev.
Performance Comparisons
AG Power drills outperform conventional drills in tool life, cutting force, and machining time. For instance, AGPSLSD drills achieve stable non-step drilling up to 7×D with tool life up to 500 holes versus about 12 holes for competitors. AGPLSD drills enable non-step drilling up to 20×D, reducing machining time by approximately 30% compared to step feed conventional drills.
Tool Life and Wear Resistance
Wear tests after hundreds of holes show minimal corner wear and optimized chip formation, contributing to longer tool life and consistent machining quality due to the AG coating and flute design.
Product Dimensions and Ordering Information
- Helix angle: 34°
- Point angle: 118°
- Diameter tolerance: h8
- Material: High alloy HSS with cobalt (Co)
Drill diameters range from approximately 1.0 mm to 20.0 mm depending on series, with detailed flute and overall lengths provided. Packaging is typically one drill per package; smaller diameters (<2.0 mm) come in sets of 10. Some products are exclusive to specific distributors in Japan.
Recommendations and Limitations
- Recommended for carbon steels, alloy steels, pre-hardened steels (up to 40–50 HRC), mold steels, cast irons, titanium alloys, and some nickel alloys.
- Not recommended for high hardness stainless steels (e.g., SUS304, SUS316) or materials above 50 HRC.
- Use water-soluble cutting fluids and vertical machining centers for optimal results.
- Reduce cutting speed and feed by 20% when using non-water-soluble fluids or machining rolled/forged surfaces.
- Employ step feeding for hole depths exceeding recommended limits, with intervals of 0.5–1×D (or 0.2–0.5×D for small diameters), returning the drill to the hole entrance between steps.
- Use collet or milling chucks for secure tool holding.
- Pre-drilling guide holes of 2–3×D depth are advised for long drills.
Operational Warnings
Adjust cutting conditions based on machine rigidity, workpiece clamping, and shape. Chip evacuation issues may require step feeding even for shallower holes. Proper coolant application and secure tool holding are critical to prevent tool damage and maintain machining quality.
Pricing and Stock Information
Pricing is listed in Japanese yen, with some items available only through designated agents in Japan. Stock availability is indicated, and packaging details are provided.
Contact and Support
Contact details for sales offices and support centers across Japan are included for assistance with cutting conditions, tool selection, pricing, and stock inquiries.
Summary
The AG Power series offers advanced coating and flute design technologies enabling high feed rates, extended tool life, and efficient chip evacuation. Covering regular, semi-long, and long drills, the series supports a wide range of hole depths and materials, providing a versatile and efficient solution for industrial drilling applications. Adherence to recommended cutting parameters, coolant use, and machining practices is essential for optimal performance.
Catalog excerpts

Fast feed high performance HSS drills AG Power Semi-long Drills AG Power Long Drills
Open the catalog to page 1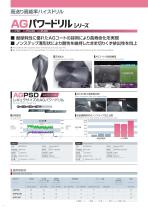
Fast-feed high performance HSS drill AGPSD AGPSLSD AGPLSD i Bisiieicanfc AG □ - MOSS iz^omm^it^mm AG coating with superior wear resistance and long tool life By flutes shape for non step drilling, to improve a cutting chips discharge performance while maintaining rigidity Cross section structure of AG coating O'-mM Excellent CJtlffl Good X:^j§ Not Used MEP(No mark):}f ISUStt^j Not Recomendec
Open the catalog to page 2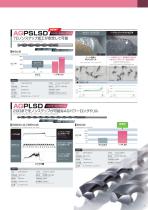
Competitor *drilling 12 holes AGPSLSD 'drilling 500 holes Stable cutting for 7D non-step drilling Comparison of tool life Feed Speed Hole Depth/Blind hole Wdrk material Cutting Fluid/Wet Machine/Vertical machining center Corner damage Chips has grown Wear of corner is small. superior to wear resistance Chips has divided and discharged well I^M0JJ£J/l.tfc$5£ Comparison of cutting force AG Power Long Drills can drills to 20xD without stepping Comparison of cutting force and time Jsual drills Cutting Speed Feed Speed
Open the catalog to page 3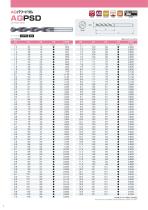
imr® n-^-iV) HM seas fauns mica Sold one per packaged Oper package it below 2.0mm)
Open the catalog to page 4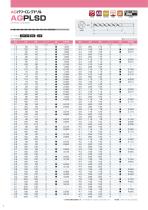
AG Power Long Drills □BtfStIlE:£E!(pp"n'"S"° Available for Japan customers only.
Open the catalog to page 6
□BtfStIlJS:£E!(pp"n'"S"° Available for Japan customers only.
Open the catalog to page 7
AG Power Long Drills
Open the catalog to page 8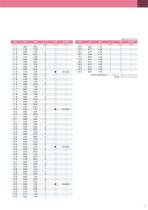
Available for Japan customers only.
Open the catalog to page 9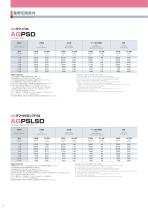
Warnings on using the drilling condition tables 1) Adjust drilling condition according to the rigidity of machine or work clamp state 2) The table values are for drilling with water soluble cutting fluid. 3) Provide sufficient amount cutting fluid to the cutting point and in the flute 4) In non water soluble cutting fluid, reduce the rotation and feed by 20% 5) A work material and drilling condition to chip removal may be worse. In that case.please add step feeding 3) In step feed, return to the entrance hole. 7) Step feed interval is about 0.5—IxD. In small diameter, about 0.2—0.5XD 3) Use a...
Open the catalog to page 10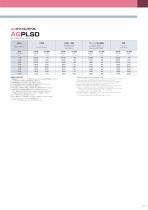
AG Power Long Drills 2) cots a*ff B*»tt« mmmm ufdi-e-w. Warnings on using the drilling condition tables I )Adjust drilling condition according to the rigidity of machine or work clamp state 2)The table values are for drilling with water soluble cutting fluid 3)Provide sufficient amount cuutting fluid to the cutting point and in the flute 4)ln non water soluble cutting fluid, reduce the rotation and feed by 20% 5)Use the table values for drilling depths under 20XD 3)When for hole depth more than 20XD reduce the rotation and feed by 30% 7)When for hole depth more than I 7XD deep, add step feediing...
Open the catalog to page 11All NACHI America catalogs and technical brochures
 AQUA Drills EX Power Feed
12 Pages
 AQUA Drills EX Series
16 Pages
 AquaREVO Drills Oil-Hole
12 Pages
 CUTTING TOOLS 2019-2020
786 Pages
 GSX MILL Roughing
4 Pages
 GSX MILL SLOT
2 Pages
 GSX MILL Series
16 Pages
 GSX MILL VL Roughing
2 Pages
 GSX MILL VL Hard
2 Pages
 GSX MILL VL Series
20 Pages
 AG Starting Drills
4 Pages
 AG-ESS DRILL‚ AG-ES DRILL
8 Pages
 SG Drill Series
12 Pages
 SG Flat Drill
4 Pages
 AQUA Drills 3Flutes
8 Pages
 AQUA Drills EX Starting
4 Pages
 AQUA Drill EX VF Series
16 Pages
 AQUA Drills EX Oil-Hole (Long)
16 Pages
 AQUA Drills EX 3Flutes Series
16 Pages
 AQUA Drill EX FLAT Series
16 Pages
 AQUA Drill EX Series
16 Pages
 MC350
2 Pages
 Ball Screw Support Bearings
6 Pages
 DLC Drill & DLC-mill Series
23 Pages
 AQUA Drills Three Flutes
8 Pages
 TOOL ENGINEERING SERVICE
8 Pages
 WAVY MILL NWEX
8 Pages
 Mold Meister Ball
4 Pages
 GS MILL Long Neck Hard Ball
8 Pages
 AG-ESS DRILL?AG-ES DRILL
4 Pages
 MQL Power Long Drill
8 Pages
 DURO-SP/V5/V2
4 Pages
 DURO-V5
2 Pages
 FM ALLOY PROVA Series
8 Pages
 DURO for cold work
8 Pages
 DURO for hot work
8 Pages
 Micron Hard
4 Pages
 Pre-Harden
8 Pages
 SPECIALTY STEELS FM ALLOY
16 Pages
 Deep-groove Ball Bearings
4 Pages
 NANO ASPHER NANO GROOVER
20 Pages
 CLEAN & THERMOTECHNOLOGY
12 Pages
 Radial Ball Bearings
4 Pages
 Cylindrical Roller Bearings
3 Pages
 Ball Screw Support Bearings
5 Pages
 Precision Rolling Bearings
78 Pages
 Spherical Roller Bearings
36 Pages
 NACHI Robot Catalog 2012
20 Pages
 ULTRA PRECISION MACHINE TOOLS
16 Pages
 MACHINE TOOLS
28 Pages
 Machining Evolution
44 Pages
 Metal Band Saw Blades
28 Pages
 AG-mill Series
20 Pages
 End Mills for Copper
12 Pages
 GS MILL Long Neck Series
16 Pages
 GS MILL Series
44 Pages
 AQUA Drill Series
44 Pages


