

SCE-R

SCE-R
- Handling: Exercise caution when removing tools from packaging to avoid dropping or contact with sharp flutes.
- Mounting: Inspect tools for damage before use and ensure they are securely mounted. Stop use immediately if abnormal chattering occurs.
- Use: Confirm tool dimensions and rotation direction. Adjust cutting conditions based on material and machine rigidity. Use safety covers and goggles to protect against flying debris and sparks.
- Regrinding: Perform regrinding timely to prevent tool breakage. Follow safety protocols for handling cobalt-containing materials.
- The SCE-R Ceramic End Mill is designed for high-efficiency machining of superalloys, achieving cutting speeds up to 800 m/min.
- Utilizes silicon nitride ceramics for heat resistance, allowing operation at temperatures exceeding 1000°C.
- Available in diameters from 6mm to 12mm, with specific flute and corner radius configurations.
- Use dry cutting methods and appropriate holders for optimal performance.
- Gradual cutting depth increase is advised to prevent tool damage.
- Maintain a finishing allowance of at least 0.2mm to account for heat-affected layers.
- Ceramic end mills offer over five times the machining performance and three times the chip removal volume compared to carbide end mills.
- For further details, contact MMC Hitachi Tool Engineering offices in Japan, Europe, USA, Mexico, China, Thailand, or India.
1. When removing tools from packaging, ensure they do not pop out or drop. Avoid direct contact with sharp cutting flutes.
2. Before use, inspect tools for damage and ensure they are securely mounted. If abnormal chattering occurs, stop the machine immediately.
3. Confirm tool dimensions and rotation direction before use. Adjust cutting conditions based on material and machine rigidity.
4. Use safety equipment like goggles and covers to protect against flying debris and potential fire hazards.
5. Do not use tools for unintended purposes.
1. Use standard cutting conditions as a starting point and adjust as necessary.
2. Employ dry cutting methods and use appropriate holders like hydro chucks.
3. Prefer continuous cutting and avoid interrupted cutting.
4. Gradually reach the set cutting depth to prevent tool damage.
5. Allow for a finishing allowance of at least 0.2 mm due to potential heat-affected layers.
1. Perform regrinding at appropriate times to prevent tool breakage.
2. Use safety covers and wear protective clothing during regrinding.
3. Handle cobalt-containing products according to local regulations.
Specifications are subject to change without notice. For more information, visit the official website or contact regional offices in Japan, Europe, USA, Mexico, China, Thailand, and India.
1. Ceramic end mills offer over five times the machining performance and three times the chip removal volume compared to carbide end mills.
2. Recommended for side milling using Ni-based superalloys.
Catalog excerpts

Av IVIOl—DIISIO The Edge To Innovation Mitsubishi Hitachi Tool Engineering, Ltd. SCE-R Ceramic End Mill Corner R type
Open the catalog to page 1
Achieves high-efficiency machining for superalloy! Achieves cutting speed of vc=800m/min.! Achieves ultra-high-efficiency machining for superalloy. The tools employ a special silicon nitride ceramics with excellent heat resistance that can withstand flute tip temperatures of more than 1000°C. Cutting can be performed at much higher speeds than are normally used. By achieving cutting in the softening temperature region of the work material, tool life is greatly improved. for Superalloy Parts processing
Open the catalog to page 2
Features Cutting P6gion of Coramic End Mill (Softening temp. region of superalloy) 700 Superalloy known as a difficult-to-cut material is a material that shows high strength even up to high temperatures, but when it reaches 1000 °C or more, the material softens. High speed cutting increases the cutting heat, and the cutting force of superalloy becomes almost the same as that of stainless steel. In other words, the ceramic end mill that enables cutting in this temperature range realizes ultra-high-efficiency machining, greatly improving tool life. Cutting region of Ceramic Enc Figure: Correlation...
Open the catalog to page 3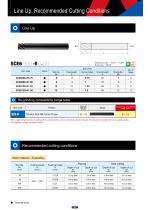
O Re-grinding compatibility range table Item Code SCE-R Product Ceramic End Mill Corner R type Line up tool dia (mm) Re-grinding compatibility range (mm) Since regrinding consists of cutting off the used section and re-manufacturing the shape, the overall tool length will be changed greatly. (For details, contact our sales office.) Work material : Superalloy Tool dia. Dc (mm) : Stocked items.
Open the catalog to page 4
Comparison of processing efficiencies of ceramicend mills and carbide end mills More' than 5 times the^ 'machining performance!!^ Wjnrhun3itmusrhuiu!uill fchipTemoval volume!! 700 600 500 400 300 200 100 0 Ceramic End Mill Carbide End Mill O Cautions on use • Dry (air blow) cutting is recommended. • Use of hydro chucks (hydraulic holders) or shrink-fit holders is recommended. • Down cutting is recommended. • Continuous cutting is recommended and interrupted cutting should be avoided as much as possible. • When tool goes into the work material, a machining method that will gradually reache the...
Open the catalog to page 5
The diagrams and table data are examples of test results, and are not guaranteed values. "Epoch" and “ ” are registered trademarks of Mitsubishi Hitachi Tool Engineering, Ltd. in Japan. Attentions on Safety 1. Cautions regarding handling (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is dropped. Be particularly careful regarding contact with the tool flutes. (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with your bare hands. 2. Cautions regarding mounting (1) Before use, check the outside...
Open the catalog to page 6All MOLDINO Tool Engineering Europe GmbH catalogs and technical brochures
 CUTTING TOOLS PRODUCTS CATALOGUE
1364 Pages
 CUTTING TOOLS PRODUCTS CATALOGUE
1056 Pages
 CBN-EPSB/CBN-EPSR
16 Pages
 EPBTS
12 Pages
 EMXR
16 Pages
 EMXA
12 Pages
 EPDRF-TH
12 Pages
 EPDBPE-ATH
20 Pages
 Epoch TH Power Mill
12 Pages
 Radius Precision ARPF
20 Pages
 Carbide Thread Mill series
16 Pages
 RV type
12 Pages
 ABPFN type
6 Pages
 TD4N type
8 Pages
 EHHB-ATH
8 Pages
 EPCDS
4 Pages
 Epoch CFRP series
6 Pages
 EPSM-PN/ EPSW-PN
32 Pages
 GALLEA series
24 Pages
 WHMB-TH
12 Pages
 EMBE-ATH/EMBPE-ATH
16 Pages
 ETR(P)-TH,ETM(LN/P)-TH
16 Pages
 EPDRE-ATH
24 Pages
 CBN-EHB
12 Pages
 EHHBE-TH3
8 Pages
 TD6N type
12 Pages
 EB4HR-ATH
12 Pages
 EHX
12 Pages
 EPHB-PN
8 Pages
 EHHRE-TH3
8 Pages
 EDT
16 Pages
 EHSE-TH
8 Pages
 NSB
12 Pages
 WHNSB-TH
20 Pages
 EMSBS
8 Pages
 Ball Precision F ABPF type
16 Pages
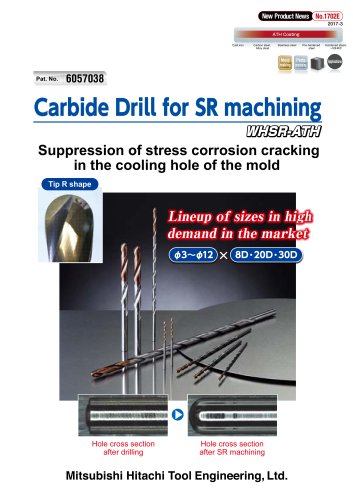 Carbide Drill for SR machining
12 Pages
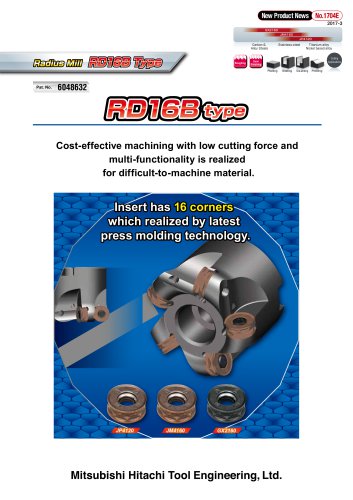 Radius Mill RD16B Type
8 Pages
 GS4TN type
4 Pages
 Red Screw Arbor
8 Pages
 ABP4F
8 Pages
 EPDBE-PN/ATH EPDSE-PN/ATH
32 Pages
 EPDBEH-TH3
20 Pages
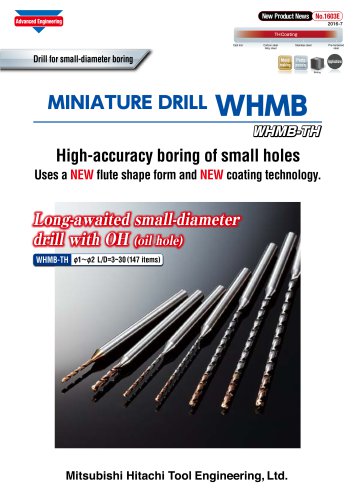 MINIATURE DRILL WHMB
8 Pages
 Epoch ® Combination Rib Ball
8 Pages
 PRODUCTS CATALOGUE 2015 - 2016
1070 Pages
 Carbide Non Step Borer series
28 Pages
 Drills for High-hardness Steels
16 Pages
 Face Mill : ASF type
8 Pages
 Face Mill : AFE45 type
8 Pages
 Ball Precision F : ABPF type
16 Pages
 Ball End Mill : ASB type
8 Pages
 Radius Precision : ARPF type
12 Pages
 Polish Mill V Type : ASPV Type
20 Pages
 Roughing End Mill : AME Type
12 Pages
 Radius Mill : AR type
20 Pages
 JM4060
4 Pages
 Epoch Micro?End Mill TH : EMM-TH
24 Pages
 Epoch Deep Radius Evolution
24 Pages
 Epoch Deep Ball Evolution Hard
16 Pages
 Epoch Micro Drill?EMD
24 Pages
 Radius Mill : ASR type
20 Pages
 Super Excellent MINI : ASM type
12 Pages
 Epoch "Mirus" Series
12 Pages
 Epoch G Turbo
8 Pages
 Roughing End Mill AME Type
12 Pages
 Z Plunging Borer?ZPB-TH
4 Pages
 Face Mill AFE45
8 Pages
 Epoch Micro Step Borer S
8 Pages











Archived catalogs
 Epoch CBN End Mill series
16 Pages
 HX3505 & HX3515
6 Pages
 GX2140
4 Pages
 Epoch "Panacea"
16 Pages
 Epoch Deep Evolution series
24 Pages
 Epoch SUS End Mill series
32 Pages
 Epoch Pencil Deep Ball Evolution
20 Pages
 Epoch Deep Radius F
12 Pages
 Re-grinding & Re-coating
20 Pages
 2009-2010 New Products Guide
5 Pages
 Micro Series for Micro Machining
14 Pages
 Milling Inserts
16 Pages
 Indexable Tools
160 Pages
 Threading Tools
6 Pages
 Turning Inserts
44 Pages
 HSS End Mills
98 Pages
 Reamers
16 Pages
 Cutters
10 Pages
 CBN End Mills
20 Pages
 Surface Treatment Tribec
8 Pages
 HSS Non Step Borer
36 Pages
 Carbide End Mills
280 Pages


- Milling tool
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Metal milling cutter
- Clamping milling cutter
- Milling cutter with cylindrical shank
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Indexable insert milling cutter
- Ball nose milling cutter
- Cutting milling cutter
- Corner radius milling cutter
- Coated milling cutter
- High-performance milling cutter