
- Catalogs
- MOLDINO Tool Engineering Europe GmbH
- ETR(P)-TH,ETM(LN/P)-TH

ETR(P)-TH,ETM(LN/P)-TH

ETR(P)-TH,ETM(LN/P)-TH
- Inspect tools for damage before use and ensure they are securely mounted.
- Stop the machine immediately if abnormal chattering occurs.
- Handle tools carefully to avoid injury, especially when removing them from packaging.
- Use safety equipment like goggles and covers during regrinding to protect against dust and flying debris.
- Follow local regulations when handling cobalt-containing tools.
- Confirm tool dimensions and rotation direction before use.
- Adjust cutting conditions based on material and machine rigidity.
- Be aware of fire risks when using oil-based coolants.
- Use tools only for their intended purpose.
- The ETR(P)-TH series features a compound neck shape for improved breakage resistance and stable deep machining.
- High-rigidity flute shapes allow for high feed rates and efficient machining.
- The oval flute cross-section reduces vibrations, enhancing cutting stability.
- Nanocomposite coating provides high temperature resistance and hardness, suitable for machining hardened steels.
- Suitable for materials like copper, carbon steel, alloy steel, stainless steel, tool steel, and hardened steel (45-65 HRC).
- Epoch Turbo Mills enable high-efficiency machining even at low rotation speeds, reducing power consumption by up to 38%.
- Regrinding and recoating services are available to maintain tool performance and extend tool life.
- Head Office: Tokyo, Japan
- International Sales: Europe, USA, Mexico, China, Thailand, India
- Materials: Hardened steels with hardness ranging from 45 to 60 HRC, including SKD61, SKT4, SKD11, and SKH51.
- Tool Types: Straight Neck, Pencil Neck, Long Neck, and Epoch Turbo Mill with various diameters and corner radii.
- Tolerances: Tolerance on corner radius is ±0.015, and on shank is h5.
- Use machines with high rigidity and accuracy.
- Adjust cutting conditions based on the machine, work material, and machining shape.
- If machine rotation speed is insufficient, reduce both rotation speed and feed rate proportionally.
- For cutting in, set the ramp introduction angle to 1° and adjust the feed rate to 60-70% of standard values.
- For tools with L/D = 15 or more, use short neck type or ball end mills to suppress chattering and stabilize cutting.
- Use appropriate coolant for the work material and machining shape.
- For high-speed conditions, use high-performance machines capable of high feed rates.
- For low load conditions, reduce cutting load by adjusting the per-flute feed rate.
- Standard conditions for low-speed use provide stable, high-efficiency cutting with long tool life.
- High-speed conditions enable ultra-high-efficiency cutting with higher feed rates.
- Low load conditions reduce cutting resistance, suitable for machines with low rigidity.
- Tool diameters range from 2mm to 20mm with corresponding corner radii.
- Overall lengths and shank diameters vary according to tool type and size.
- Specific item codes and stock sizes are provided for each tool type.
- Revolution speeds and feed rates are specified for different tool diameters and materials.
- Feed per tooth values are provided for various machining conditions.
- Recommendations for depth of cut and overhung conditions are detailed.
Catalog excerpts
M IVIOI—DIISIO The Edge To Innovation Small-diameter deep-cutting corner radius end mill for high-efficient machining Epoch Turbo Rib & Epoch Turbo Mill Mitsubishi Hitachi Tool Engineering, Ltd. New Product News No.0801E-8 20 1 9 -4
Open the catalog to page 1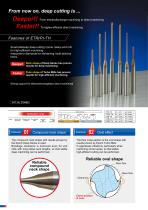
From now on, deep cutting is ... Deeper!! From electrodischarge machining to direct machining Faster!! To higher-efficient direct machining Features of ETR(P)-TH Small-diameter deep-cutting corner radius end mill for high-efficient machining responds to demands for shortening mold delivery times. Neck shape of Deep Series has proven results for deep machining. Flute shape of Turbo Mills has proven results for high-efficient machining. Strong support for electrodischargeless direct machining! Application range Copper Carbon steel Alloy steel Stainless steel Pre-hardened Tool steel steel Mold making...
Open the catalog to page 2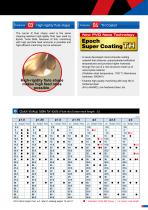
Features 03 High-rigidity flute shape The corner R flute shape used is the same chipping-resistant high-rigidity flute type used by Epoch Turbo Mills. Because of this, machining with high per-flute feed amounts is possible and high-efficient machining can be achieved. Super CoatingTfTjG • A newly developed nanocomposite coating material that achieves unprecedented withstand temperatures and provides higher hardness through the use of a new structure made up of nanocrystal material. (Oxidation start temperature: 1100° C; Membrane hardness: 3600HV) high feed ossible • Enables high-quality machining...
Open the catalog to page 3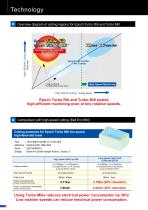
Technology Overview diagram of cutting regions for Epoch Turbo Rib and Turbo Mill Epoch Epoch Turbo Mill Power Ball (Feed rate) High Efficient Cutting Low revolution & High feed cutting. New machining area General Ball End Mill 一般ボールエン ドミル (TiAlN Coated) (TiAlNコーテ ィング) Long overhang (Cutting area by low rev.) High Speed Cutting High Speed Machining (Cutting Speed) Epoch Turbo Rib and Turbo Mill enable high-efficient machining even at low rotation speeds. Comparison with high-speed cutting (Ball End Mill) Cutting examples for Epoch Turbo Mill low-speed, high-feed-rate tools Tool : φ10 Ball End...
Open the catalog to page 4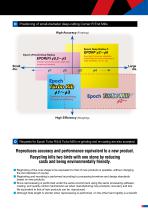
High Accuracy (Finishing) High Efficiency (Roughing) Reproduces accuracy and performance equivalent to a new product. Recycling kills two birds with one stone by reducing costs and being environmentally friendly. ■ Regrinding of the oval shape to be equivalent to that of new products is possible, without changing the tool diameter of course. ■ Regrinding and recoating is performed according to processing knowhow and design standards based on new products. ■ Since reprocessing is performed under the same environment using the same processing software, coating, and quality control mechanisms as...
Open the catalog to page 5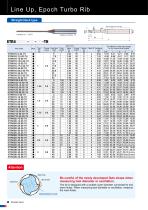
Straight Neck type Attention Be careful of the newly developed flute shape when measuring tool diameter or oscillation. The bit is designed with a smaller outer diameter connected to end slave flutes. When measuring tool diameter or oscillation, measure the main flutes.
Open the catalog to page 6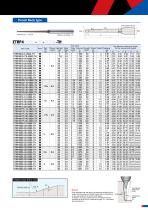
Pencil Neck type ETRP4 OOOO -00-0000 -TH Item Code
Open the catalog to page 7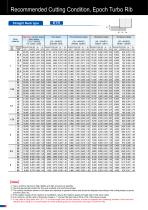
Straight Neck type ETR [Note] © Use a machine having as high rigidity and high accuracy as possible. @ Use the appropriate coolant for the work material and machining shape. ® The cutting conditions shown in this table are intended as general criteria and should be adjusted according to the cutting shape, purpose, machine used, etc. ® If the rotation speed of the machine is insufficient, reduce the rotation speed and feed rate by the same ratios. © For cutting in, set the ramp introduction angle to 1° and set the feed rate to 60 to 70% of the above values. © In the case of using tools with...
Open the catalog to page 8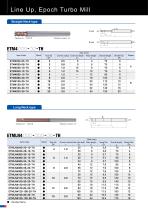
Straight Neck type Long Neck type
Open the catalog to page 10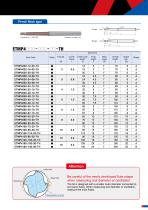
Pencil Neck type Be careful of the newly developed flute shape when measuring tool diameter or oscillation. The bit is designed with a smaller outer diameter connected to end slave flutes. When measuring tool diamet
Open the catalog to page 11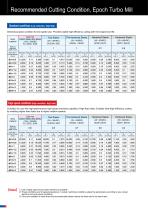
General-purpose condition for low-speed use. Provides stable high-efficiency cutting with the longest tool life. [Note] © Use a highly rigid and accurate machine as possible. © These conditions are for general guidance; in actual machining conditions adjust the parameters according to your actual machine and work-piece conditions. © If the rpm available is lower than that recommended please reduce the feed rate to the same ratio.
Open the catalog to page 12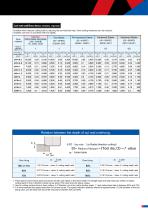
Condition which reduces cutting load by reducing the per-flute feed rate. Since cutting resistance can be reduced, it enables use even on machines with low rigidity. ® Feed rates for pencil-neck types are shown for 6Dc and higher in the above table. For straight type and long-neck type of 6Dc or higher, cutting depth in the Z direction should be set about 10% lower than the above values. © Use for cutting contour lines or down cutting. In Z direction, cut at an incline (incline angle: 1 °and reduce feed rate to between 60% and 70%. © It is recommended that speed reduction for corners be set....
Open the catalog to page 13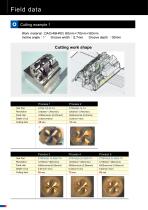
Field data Cutting example 1 Work material : DAC(48HRC) 60mm×70mm×50mm Incline angle:1° Groove width :2.7mm Groove depth :30mm Cutting work shape Feed rate Cutting time Use Tool Revolution Feed rate Cutting time
Open the catalog to page 14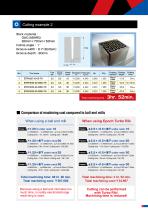
Cutting example 2 Work material: DAC(48HRC) 80mm×70mm×50mm Incline angle:1° Groove width:2.7 (Bottom) Groove depth:30mm Tool name Under Revolution Feed rate neck min-1 mm/min Total machining time : Cooling Cutting method depth Water base Water base Water base Water base Cutting time ■ Comparison of machining cost compared to ball end mills When using a ball end mill Process 1 When using Epoch Turbo Rib Total machining time: 80 hr. 26 min. Total machining cost: ¥567,060
Open the catalog to page 15
The diagrams and table data are examples of test results, and are not guaranteed values. "Epoch" and “ ” are registered trademarks of Mitsubishi Hitachi Tool Engineering, Ltd. in Japan. Attentions on Safety 1. Cautions regarding handling (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is dropped. Be particularly careful regarding contact with the tool flutes. (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with your bare hands. 2. Cautions regarding mounting (1) Before use, check the outside...
Open the catalog to page 16All MOLDINO Tool Engineering Europe GmbH catalogs and technical brochures
 CUTTING TOOLS PRODUCTS CATALOGUE
1364 Pages
 CUTTING TOOLS PRODUCTS CATALOGUE
1056 Pages
 CBN-EPSB/CBN-EPSR
16 Pages
 EPBTS
12 Pages
 EMXR
16 Pages
 EMXA
12 Pages
 EPDRF-TH
12 Pages
 EPDBPE-ATH
20 Pages
 Epoch TH Power Mill
12 Pages
 Radius Precision ARPF
20 Pages
 Carbide Thread Mill series
16 Pages
 SCE-R
6 Pages
 RV type
12 Pages
 ABPFN type
6 Pages
 TD4N type
8 Pages
 EHHB-ATH
8 Pages
 EPCDS
4 Pages
 Epoch CFRP series
6 Pages
 EPSM-PN/ EPSW-PN
32 Pages
 GALLEA series
24 Pages
 WHMB-TH
12 Pages
 EMBE-ATH/EMBPE-ATH
16 Pages
 EPDRE-ATH
24 Pages
 CBN-EHB
12 Pages
 EHHBE-TH3
8 Pages
 TD6N type
12 Pages
 EB4HR-ATH
12 Pages
 EHX
12 Pages
 EPHB-PN
8 Pages
 EHHRE-TH3
8 Pages
 EDT
16 Pages
 EHSE-TH
8 Pages
 NSB
12 Pages
 WHNSB-TH
20 Pages
 EMSBS
8 Pages
 Ball Precision F ABPF type
16 Pages
 Carbide Drill for SR machining
12 Pages
 Radius Mill RD16B Type
8 Pages
 GS4TN type
4 Pages
 Red Screw Arbor
8 Pages
 ABP4F
8 Pages
 EPDBE-PN/ATH EPDSE-PN/ATH
32 Pages
 EPDBEH-TH3
20 Pages
 MINIATURE DRILL WHMB
8 Pages
 Epoch ® Combination Rib Ball
8 Pages
 PRODUCTS CATALOGUE 2015 - 2016
1070 Pages
 Carbide Non Step Borer series
28 Pages
 Drills for High-hardness Steels
16 Pages
 Face Mill : ASF type
8 Pages
 Face Mill : AFE45 type
8 Pages
 Ball Precision F : ABPF type
16 Pages
 Ball End Mill : ASB type
8 Pages
 Radius Precision : ARPF type
12 Pages
 Polish Mill V Type : ASPV Type
20 Pages
 Roughing End Mill : AME Type
12 Pages
 Radius Mill : AR type
20 Pages
 JM4060
4 Pages
 Epoch Micro?End Mill TH : EMM-TH
24 Pages
 Epoch Deep Radius Evolution
24 Pages
 Epoch Deep Ball Evolution Hard
16 Pages
 Epoch Micro Drill?EMD
24 Pages
 Radius Mill : ASR type
20 Pages
 Super Excellent MINI : ASM type
12 Pages
 Epoch "Mirus" Series
12 Pages
 Epoch G Turbo
8 Pages
 Roughing End Mill AME Type
12 Pages
 Z Plunging Borer?ZPB-TH
4 Pages
 Face Mill AFE45
8 Pages
 Epoch Micro Step Borer S
8 Pages











Archived catalogs
 Epoch CBN End Mill series
16 Pages
 HX3505 & HX3515
6 Pages
 GX2140
4 Pages
 Epoch "Panacea"
16 Pages
 Epoch Deep Evolution series
24 Pages
 Epoch SUS End Mill series
32 Pages
 Epoch Pencil Deep Ball Evolution
20 Pages
 Epoch Deep Radius F
12 Pages
 Re-grinding & Re-coating
20 Pages
 2009-2010 New Products Guide
5 Pages
 Micro Series for Micro Machining
14 Pages
 Milling Inserts
16 Pages
 Indexable Tools
160 Pages
 Threading Tools
6 Pages
 Turning Inserts
44 Pages
 HSS End Mills
98 Pages
 Reamers
16 Pages
 Cutters
10 Pages
 CBN End Mills
20 Pages
 Surface Treatment Tribec
8 Pages
 HSS Non Step Borer
36 Pages
 Carbide End Mills
280 Pages


- Milling tool
- Chuck
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Metal milling cutter
- Clamping milling cutter
- Milling cutter with cylindrical shank
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Indexable insert milling cutter
- Ball nose milling cutter
- Cutting milling cutter
- Corner radius milling cutter
- Coated milling cutter
- High-performance milling cutter