

EHSE-TH

EHSE-TH
- 20° helix angle and integral shank with thick web thickness.
- Four guides with double margins to reduce cutting resistance and prevent deflection and chipping.
- Chamfered cutting edge to moderate stress concentration, preventing cracks and improving tool life.
- TH coating for enhanced surface hardness and heat resistance.
- Inspect for damage before use and ensure secure mounting.
- Stop machine if abnormal chattering occurs.
- Wear safety equipment and ensure safety cover during regrinding.
- Handle tools carefully to avoid contact with sharp flutes.
- Use standard cutting conditions table, adjust for large depths or low machine rigidity.
- Ensure sufficient cutting fluid supply.
- Regrind drill as necessary, consider professional services.
Catalog excerpts
Carbide Drill for Hardened Steel Epoch TH Hard Drill
Open the catalog to page 1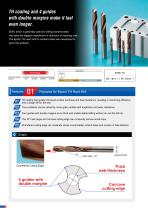
TH coating and 4 guides with double margins make it last even longer. EDM, which is generally used for drilling hardend steel, has been the biggest impediment to reduction of maching cost. The Epoch TH Hard Drill for hardend steel was developed to solve this problem. TH Coating Carbon steel Tool steel Alloy steel Pre-hardened steel Hardened steel Hardened steel Hardened steel 45~55HRC 55~65HRC 65~72HRC Mold making EHSE-TH Parts processing Features for Epoch TH Hard Drill TH coating has greatly improved surface hardness and heat resistance, resulting in machining efficiency and a longer life for...
Open the catalog to page 2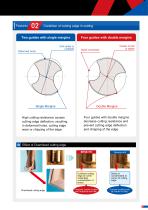
Condition of cutting edge in cutting Two guides with single margine Deformed circle Drill center is unstable Four guides with double margins Center of drill is stable Good roundness Single Margine Double Margine High cutting resistance causes cutting edge deflection, resulting in deformed holes, cutting edge wear or chipping of the edge. Four guides with double margins decrease cutting resistance and prevent cutting edge deflection and chipping of the edge. Effect of Chamfered cutting edge EHSE-TH Confered cutting edge at corner moderates concentration of stress. Chamfered cutting edge General...
Open the catalog to page 3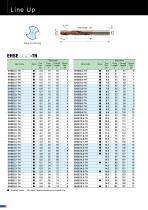
EHSE Item Code : Stocked Items. No mark : Manufactured upon request only
Open the catalog to page 4
[Note] 1. The above conditions apply to a hole-depth of 3 times the diameter or less. 2. Mount the drill on a collet without any flaws. Adjust the drill run out to 0.02mm or less. 3. Use a machine with high rigidity. 4. Supply a sufficient amount of cutting fluid (Water-soluble, dilution of 20 times or less) to machining points. © The above conditions apply to a hole-depth of 3 times the diameter or less. © Cutting performance may vary according to the material being cut and its hardness. © Mount the drill on a collet without any flaws. Adjust the drill run out to 0.02mm or less. @ Supply a sufficient...
Open the catalog to page 5
O Drilling for Machine parts Work material Machine parts SKD61 (52HRC) 06 Cutting Conditions Item Code : EHSE6.0-TH vc=30m/min n = 1,592min-1 f=0.12mm/rev v f=191mm/min Cutting fluid: Water-soluble coolant Machine : M/C EHSE -TH Conventional ■ Cutting edge condition after drilling 150 holes Drilling for Cold work die steel Work material Cold Work Die Steel SKD11 (60HRC) Cutting Conditions EHSE -TH Conventional Tool life 4.8 times longer ■ Cutting edge condition after drilling 100 holes Coarse chips
Open the catalog to page 6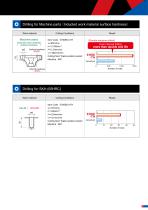
Work material Cutting Conditions Machine parts /Inducted work material surface hardness Item Code : EHSE6.0-TH vc=60m/min n = 3,180mim1 f=0.12mm/rev v f=382mm/min Cutting fluid: Water-soluble coolant Machine : M/C [Double margine effect] Even interrupt drilling more than double tool life EHSE -TH Conventional O Drilling for SKH (65HRC) Work material Cutting Conditions Item Code : EHSE6.0-TH vc=10m/min n = 530min-1 f=0.04mm/rev v f=21mm/min Cutting fluid: Water-soluble coolant Machine : M/C EHSE -TH Conventional
Open the catalog to page 7
The diagrams and table data are examples of test results, and are not guaranteed values. "Epoch" , “ ” and “ ” are registered trademarks of Mitsubishi Hitachi Tool Engineering, Ltd. in Japan. Attentions on Safety 1. Cautions regarding handling (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is dropped. Be particularly careful regarding contact with the tool flutes. (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with your bare hands. 2. Cautions regarding mounting (1) Before use, check the...
Open the catalog to page 8All MOLDINO Tool Engineering Europe GmbH catalogs and technical brochures
 CUTTING TOOLS PRODUCTS CATALOGUE
1364 Pages
 CUTTING TOOLS PRODUCTS CATALOGUE
1056 Pages
 CBN-EPSB/CBN-EPSR
16 Pages
 EPBTS
12 Pages
 EMXR
16 Pages
 EMXA
12 Pages
 EPDRF-TH
12 Pages
 EPDBPE-ATH
20 Pages
 Epoch TH Power Mill
12 Pages
 Radius Precision ARPF
20 Pages
 Carbide Thread Mill series
16 Pages
 SCE-R
6 Pages
 RV type
12 Pages
 ABPFN type
6 Pages
 TD4N type
8 Pages
 EHHB-ATH
8 Pages
 EPCDS
4 Pages
 Epoch CFRP series
6 Pages
 EPSM-PN/ EPSW-PN
32 Pages
 GALLEA series
24 Pages
 WHMB-TH
12 Pages
 EMBE-ATH/EMBPE-ATH
16 Pages
 ETR(P)-TH,ETM(LN/P)-TH
16 Pages
 EPDRE-ATH
24 Pages
 CBN-EHB
12 Pages
 EHHBE-TH3
8 Pages
 TD6N type
12 Pages
 EB4HR-ATH
12 Pages
 EHX
12 Pages
 EPHB-PN
8 Pages
 EHHRE-TH3
8 Pages
 EDT
16 Pages
 NSB
12 Pages
 WHNSB-TH
20 Pages
 EMSBS
8 Pages
 Ball Precision F ABPF type
16 Pages
 Carbide Drill for SR machining
12 Pages
 Radius Mill RD16B Type
8 Pages
 GS4TN type
4 Pages
 Red Screw Arbor
8 Pages
 ABP4F
8 Pages
 EPDBE-PN/ATH EPDSE-PN/ATH
32 Pages
 EPDBEH-TH3
20 Pages
 MINIATURE DRILL WHMB
8 Pages
 Epoch ® Combination Rib Ball
8 Pages
 PRODUCTS CATALOGUE 2015 - 2016
1070 Pages
 Carbide Non Step Borer series
28 Pages
 Drills for High-hardness Steels
16 Pages
 Face Mill : ASF type
8 Pages
 Face Mill : AFE45 type
8 Pages
 Ball Precision F : ABPF type
16 Pages
 Ball End Mill : ASB type
8 Pages
 Radius Precision : ARPF type
12 Pages
 Polish Mill V Type : ASPV Type
20 Pages
 Roughing End Mill : AME Type
12 Pages
 Radius Mill : AR type
20 Pages
 JM4060
4 Pages
 Epoch Micro?End Mill TH : EMM-TH
24 Pages
 Epoch Deep Radius Evolution
24 Pages
 Epoch Deep Ball Evolution Hard
16 Pages
 Epoch Micro Drill?EMD
24 Pages
 Radius Mill : ASR type
20 Pages
 Super Excellent MINI : ASM type
12 Pages
 Epoch "Mirus" Series
12 Pages
 Epoch G Turbo
8 Pages
 Roughing End Mill AME Type
12 Pages
 Z Plunging Borer?ZPB-TH
4 Pages
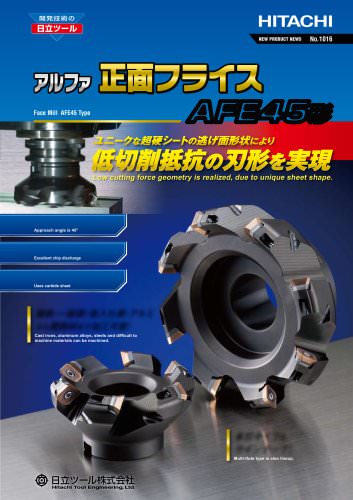 Face Mill AFE45
8 Pages
 Epoch Micro Step Borer S
8 Pages











Archived catalogs
 Epoch CBN End Mill series
16 Pages
 HX3505 & HX3515
6 Pages
 GX2140
4 Pages
 Epoch "Panacea"
16 Pages
 Epoch Deep Evolution series
24 Pages
 Epoch SUS End Mill series
32 Pages
 Epoch Pencil Deep Ball Evolution
20 Pages
 Epoch Deep Radius F
12 Pages
 Re-grinding & Re-coating
20 Pages
 2009-2010 New Products Guide
5 Pages
 Micro Series for Micro Machining
14 Pages
 Milling Inserts
16 Pages
 Indexable Tools
160 Pages
 Threading Tools
6 Pages
 Turning Inserts
44 Pages
 HSS End Mills
98 Pages
 Reamers
16 Pages
 Cutters
10 Pages
 CBN End Mills
20 Pages
 Surface Treatment Tribec
8 Pages
 HSS Non Step Borer
36 Pages
 Carbide End Mills
280 Pages


- Milling tool
- Chuck
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Metal milling cutter
- Clamping milling cutter
- Milling cutter with cylindrical shank
- End mill
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Indexable insert milling cutter
- Ball nose milling cutter
- Cutting milling cutter
- Corner radius milling cutter
- Coated milling cutter
- High-performance milling cutter