

EDT

EDT
- Handling: Exercise caution when removing tools from packaging to avoid injury from sharp edges.
- Mounting: Ensure tools are free from defects and securely mounted before use.
- Usage: Confirm tool dimensions and rotation direction. Adjust cutting conditions based on material and machine rigidity. Use safety equipment to prevent injury from flying debris.
- Regrinding: Perform regrinding at appropriate times to prevent tool breakage. Follow local regulations for handling cobalt and its compounds.
- Tools are designed to reduce the risk of breakage and improve chip evacuation.
- Thread milling can be performed without synchronizing rotation and feed rates, similar to end mills.
- Tools can handle right-hand, left-hand, and fine thread milling by changing the NC program.
- Minimal incomplete threads allow for milling to the bottom of shallow holes.
Catalog excerpts

Carbide Threading tool ET-PN EDT-TH EDT-m-m Carbide Thread Mill series Mitsubishi Hitachi Tool Engineering, Ltd. |~N~ew Product News | No.1305E-3 | 201 7-6 |
Open the catalog to page 1
Features Applications Applicable range Cast iron Carbon steel Alloy steep Tool steel Pre-hardened Hardened steel steel 45~55HRC Mold making ET-PN EDT-TH, EDT-(N)PT-ATH Parts processing Features of Epoch Thread Mill ・Tough and strong edge design provides threading of hardened steels. st ・Tip shape that reduces cutting resistance suppresses tool bending. ・Drastically reduces tool breakage, Reduces risk a particular problem New coating with excellent adhesion and wear resustance ecnatsuser raew dna noisehda tnellecxe htiw gnitaoc weN ecnatsuser raew dna noisehda tnellecxe htiw gnitaoc weN ecnatsuser...
Open the catalog to page 2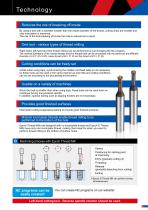
Te c h n o l o g y Reduces the risk of breaking off inside By using a tool with a diameter smaller than the inside diameter of the thread, cutting chips are smaller and chip evacuation is improved. The risk of the tool breaking off inside the hole is reduced as a result. One tool - various types of thread milling Right hand, left-hand and fine thread milling can be performed by just changing the NC program. The nominal diameters of the coarse threads and fine threads that can be processed with the same tool are different. (Example: For ET-1.25-16-PN, coarse thread is M8 × P1.25 and fine thread...
Open the catalog to page 3
: Stocked items, □: Stocked by specified distributor. Contact with our sales department, ^For information abo
Open the catalog to page 4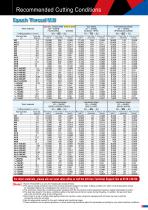
©Epoch Thread Mill Is an only for threading the inside of holes, ©The above cutting conditions are for the nominal diameters stated in the table, Cutting conditions for other nominal diameters should be calculated taking into consideration the cautions on use (p,15), ©The machinery should be a machining center equipped with NC (numerical control) equipment having a helical interpolation function, ©The feed rate stated in the above conditions table is the feed rate at the tool center during threading, In addition, the per-tooth feed rate is the numerical value at the cutting point, ©Since there...
Open the catalog to page 5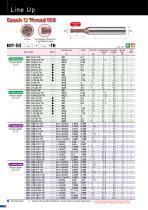
EDT-(U) . - . -TH .J : Stocked Items, □: Stocked by specified distributor. Contact with our sales department, *^For information ab
Open the catalog to page 6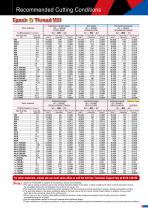
©Epoch D Thread Mill Is capable of simultaneous boring and threading, ©The above cutting conditions are for the nominal diameters stated in the table, Cutting conditions for other nominal diameters should be calculated taking into consideration the cautions on use (p, 15). ©The machinery should be a machining center equipped with NC (numerical control) equipment having a helical interpolation function, ©The feed rate stated in the above conditions table is the feed rate at the tool center during thread milling, In addition, the per-tooth feed rate is the numerical value at the cutting point, ©Since...
Open the catalog to page 7
Thread Mill fo PT,NPT for PT,NPT for PT,NPT T,NPT N Threads Th ead Threads Left-hand edge θn φDs 1 incomplete thread and 2 complete threads Item code Pilot hole Pilot hole required not required (pilot hole diameter) Reference Under neck Overall tool dia. length length R2 Dc L Nominal diameter correction amount Nominal diameter correction amount Item code Neck angle θ n: 1.7° ※The neck angle (θ n) of EDT-PT1(NPT1)-45-ATH is 0° (straight neck). Pilot hole Pilot hole required not required (pilot hole diameter) Reference Under neck Overall tool dia. length length R2 Dc L ●:Stocked Items. Nominal...
Open the catalog to page 8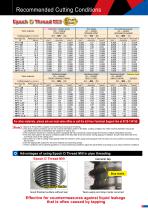
Work material For other materials, please ask our local sales office or call the toll-free Technical Support line at 0120-134159. [Nofa ©Epoch D Thread Mill Is capable of simultaneous boring and threading, ©The above cutting conditions are for the nominal diameters stated in the table, Cutting conditions for other nominal diameters should be calculated taking into consideration the cautions on use (p,15), ©The machinery should be a machining center equipped with NC (numerical control) equipment having a helical interpolation function, ©The feed rate stated in the above conditions table is the...
Open the catalog to page 9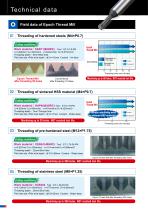
Te c h n i c a l d a t a Field data of Epoch Thread Mill 01 Threading of hardened steels (M4×P0.7) Cutting conditions Work material:SKD11(60HRC) Tool:ET-0.7-8-PN n= 4,620min-1(vc=45m/min) v f =62mm/min(f z =0.015mm/t) Threading depth:8mm Blind hole Pilot hole dia.×Pilot hole depth: φ3.4 ×12mm Coolant:Air-blow Epoch Thread Mill Damaged on 10th hole Threading hole count (holes) Epoch Thread Mill after threading 50 holes Conventional after threading 10 holes. Machining up to 50 holes. NOT reached tool life. 02 Threading of sintered HSS material (M4×P0.7) Cutting conditions Work material:HAP40(64HRC)...
Open the catalog to page 10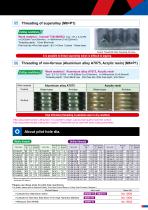
05 Threading of superalloy (M6xP1) Culling conditions'll/ Work material : inconel 718(40HRC) Tool: et-i.0-12-pn n =2,420min-1(vc=35m/min) vf=56mm/min (fz=0.025mm/t) Threading depth : 12mm Blind hole Pilot hole dia.xPilot hole depth : 05.1x15mm Coolant : Water-base it is possible to thread superalloy which is difficult to tapping. 06 Threading of non-ferrous (Aluminium alloy A7075, Acrylic resin) (M6xP1) Work material : Aluminium alloy A7075, Acrylic resin Tool : ET-1.0-12-PN n=14,500min-1(vc=210m/min) vf=540mm/min (fz=0.04mm/t) Threading depth : 12mm Blind hole Pilot hole dia.xPilot hole depth...
Open the catalog to page 11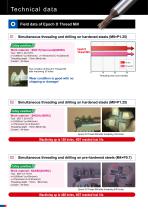
Te c h n i c a l d a t a Field data of Epoch D Thread Mill Simultaneous threading and drilling on hardened steels (M8×P1.25) Cutting conditions Work material:SKD11(Improved)(62HRC) Tool:EDT-1.25-16-TH n =2,060min-1(vc=40m/min) v f =47mm/min z =0.025mm/t) (f Threading depth:15mm Blind hole Coolant:Air-blow Epoch D Thread Mill Tool condition of Epoch D Thread Mill after machining 30 holes Wear condition is good with no chipping or damage! Threading hole count (holes) Simultaneous threading and drilling on hardened steels (M8×P1.25) Cutting conditions Work material:SKD61(45HRC) Tool:EDT-1.25-16-TH ...
Open the catalog to page 12All MOLDINO Tool Engineering Europe GmbH catalogs and technical brochures
 CUTTING TOOLS PRODUCTS CATALOGUE
1364 Pages
 CUTTING TOOLS PRODUCTS CATALOGUE
1056 Pages
 CBN-EPSB/CBN-EPSR
16 Pages
 EPBTS
12 Pages
 EMXR
16 Pages
 EMXA
12 Pages
 EPDRF-TH
12 Pages
 EPDBPE-ATH
20 Pages
 Epoch TH Power Mill
12 Pages
 Radius Precision ARPF
20 Pages
 Carbide Thread Mill series
16 Pages
 SCE-R
6 Pages
 RV type
12 Pages
 ABPFN type
6 Pages
 TD4N type
8 Pages
 EHHB-ATH
8 Pages
 EPCDS
4 Pages
 Epoch CFRP series
6 Pages
 EPSM-PN/ EPSW-PN
32 Pages
 GALLEA series
24 Pages
 WHMB-TH
12 Pages
 EMBE-ATH/EMBPE-ATH
16 Pages
 ETR(P)-TH,ETM(LN/P)-TH
16 Pages
 EPDRE-ATH
24 Pages
 CBN-EHB
12 Pages
 EHHBE-TH3
8 Pages
 TD6N type
12 Pages
 EB4HR-ATH
12 Pages
 EHX
12 Pages
 EPHB-PN
8 Pages
 EHHRE-TH3
8 Pages
 EHSE-TH
8 Pages
 NSB
12 Pages
 WHNSB-TH
20 Pages
 EMSBS
8 Pages
 Ball Precision F ABPF type
16 Pages
 Carbide Drill for SR machining
12 Pages
 Radius Mill RD16B Type
8 Pages
 GS4TN type
4 Pages
 Red Screw Arbor
8 Pages
 ABP4F
8 Pages
 EPDBE-PN/ATH EPDSE-PN/ATH
32 Pages
 EPDBEH-TH3
20 Pages
 MINIATURE DRILL WHMB
8 Pages
 Epoch ® Combination Rib Ball
8 Pages
 PRODUCTS CATALOGUE 2015 - 2016
1070 Pages
 Carbide Non Step Borer series
28 Pages
 Drills for High-hardness Steels
16 Pages
 Face Mill : ASF type
8 Pages
 Face Mill : AFE45 type
8 Pages
 Ball Precision F : ABPF type
16 Pages
 Ball End Mill : ASB type
8 Pages
 Radius Precision : ARPF type
12 Pages
 Polish Mill V Type : ASPV Type
20 Pages
 Roughing End Mill : AME Type
12 Pages
 Radius Mill : AR type
20 Pages
 JM4060
4 Pages
 Epoch Micro?End Mill TH : EMM-TH
24 Pages
 Epoch Deep Radius Evolution
24 Pages
 Epoch Deep Ball Evolution Hard
16 Pages
 Epoch Micro Drill?EMD
24 Pages
 Radius Mill : ASR type
20 Pages
 Super Excellent MINI : ASM type
12 Pages
 Epoch "Mirus" Series
12 Pages
 Epoch G Turbo
8 Pages
 Roughing End Mill AME Type
12 Pages
 Z Plunging Borer?ZPB-TH
4 Pages
 Face Mill AFE45
8 Pages
 Epoch Micro Step Borer S
8 Pages











Archived catalogs
 Epoch CBN End Mill series
16 Pages
 HX3505 & HX3515
6 Pages
 GX2140
4 Pages
 Epoch "Panacea"
16 Pages
 Epoch Deep Evolution series
24 Pages
 Epoch SUS End Mill series
32 Pages
 Epoch Pencil Deep Ball Evolution
20 Pages
 Epoch Deep Radius F
12 Pages
 Re-grinding & Re-coating
20 Pages
 2009-2010 New Products Guide
5 Pages
 Micro Series for Micro Machining
14 Pages
 Milling Inserts
16 Pages
 Indexable Tools
160 Pages
 Threading Tools
6 Pages
 Turning Inserts
44 Pages
 HSS End Mills
98 Pages
 Reamers
16 Pages
 Cutters
10 Pages
 CBN End Mills
20 Pages
 Surface Treatment Tribec
8 Pages
 HSS Non Step Borer
36 Pages
 Carbide End Mills
280 Pages


- Milling tool
- Chuck
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Metal milling cutter
- Clamping milling cutter
- Milling cutter with cylindrical shank
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Indexable insert milling cutter
- Ball nose milling cutter
- Cutting milling cutter
- Corner radius milling cutter
- Coated milling cutter
- High-performance milling cutter