
- Catalogs
- MOLDINO Tool Engineering Europe GmbH
- Carbide Drill for SR machining

Carbide Drill for SR machining
Carbide Drill for SR machining
The document introduces the WHSR-ATH carbide drill, emphasizing its high market demand for SR machining. The drill features an ATH coating to reduce stress corrosion cracking in mold cooling holes.
Specifications
The drill is available in sizes from φ3 to φ12 with lengths of 8D, 20D, and 30D. It is compatible with materials such as carbon steel, alloy steel, cast iron, stainless steel, pre-hardened steel, and hardened steels up to 50HRC.
Performance Comparison
The WHSR-ATH drill surpasses traditional gundrills, offering over five times the machining performance and more than 30 times the tool life. It maintains a hole surface roughness of 4μm or less for over 100 holes.
Safety and Handling
Safety measures include inspecting the tool for damage, halting the machine if abnormal chattering occurs, and ensuring proper regrinding. Protective gear such as goggles is recommended to guard against flying debris.
Regrinding and Maintenance
Timely regrinding is crucial to prevent tool breakage. The document stresses handling cobalt-containing tools per local regulations.
Cutting Conditions
Standard cutting conditions are outlined, with recommendations for adjustments based on machining specifics. Internal coolant pressure guidelines are also provided.
Applications
The drill is ideal for parts processing and mold making, reducing scratches and stress corrosion cracking in cooling holes, thus extending mold life.
Contact Information
Contact details for international sales offices in Japan, Europe, the USA, China, Thailand, and India are included for further inquiries.
Details are provided for drilling with KDA1S(A) material using the 20WHSR1150-ATH tool. Cutting speed is set at 70m/min with feed rates of 111mm/min at the entrance, 223mm/min in the middle, and 45mm/min at the hole bottom. The tool operates on a horizontal MC machine with water-based coolant at 2.2MPa.
Machining Performance
The tool can machine over 100 holes with a surface roughness of Rz 1.5 µm. Flank wear is noted at 0.20mm, indicating when a tool change is needed.
Recommendations and Countermeasures
Issues like excessive feed, tool wear, and insufficient rpm are addressed with countermeasures such as adjusting feed rates and optimizing hole diameters.
Safety and Handling Instructions
Emphasizes safety precautions, including tool inspection, wearing safety gear, and careful handling to prevent injury. Proper regrinding practices are advised to avoid tool breakage and comply with hazardous substance regulations.
Product Information
Information on the WHSR-ATH carbide drill for SR machining is provided, suitable for various steels and cast iron. Contact information for international sales offices is included, with a note that product specifications may change without notice.
Catalog excerpts
ATH Coating Cast iron Carbon steel, Alloy steel Stainless steel Mold making Pre-hardened steel Parts processing Carbide Drill for SR machining WHSR-ATH Suppression of stress corrosion cracking in the cooling hole of the mold Tip R shape Lineup of sizes in high demand in the market φ3~φ 12 Hole cross section after drilling Hole cross section after SR machining
Open the catalog to page 1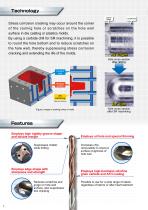
Technology corner edge Stress corrosion cracking may occur around the corner of the cooling hole or scratches on the hole wall surface in die casting or plastics molds. By using a carbide drill for SR machining, it is possible to round the hole bottom and to reduce scratches on the hole wall, thereby suppressing stress corrosion cracking and extending the life of the molds. Rz 13μm Hole cross section after drilling Coolant hole Molding portion SR machining (Sphere Radius) Figure: Image of cooling holes of mold Rz 2μm Hole cross section after SR machining Features Employs high rigidity groove...
Open the catalog to page 2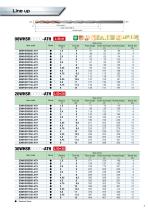
: Stocked items.
Open the catalog to page 3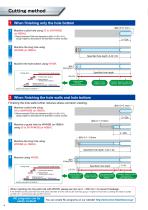
Cutting method 1 When finishing only the hole bottom 1 Machine a pilot hole using 03 to 05WHNSB (or NSBH). ※Recommended Pilot hole diameter is φDc (+0.03~+0.1). Gurge might be decreased if the diameter is same as φDc. 2 Machine the long hole using WHNSB (or NSBH). Specified hole depth -0.42×Dc 3 Machine the hole bottom using WHSR. (Drilling dia.) Inching dwell Specified hole depth Feed rate at hole middle section Inching return amount Inching amount + Inching return amount Inching feed for hole bottom R section Inching amount + Inching return amount:2000mm/min Feed for hole middle section Insertion...
Open the catalog to page 4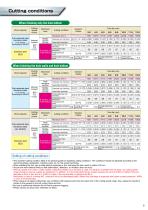
Cutting conditions When finishing only the hole bottom
Open the catalog to page 5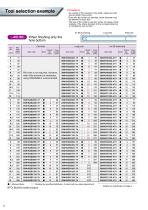
Tool selection ^Cautions •As a guide of the maximum hole depth, please set with groove length minus 2xDc. •Even with the same tool diameter, shank diameter may be different for each tool. •The size of the collet to use also varies, so please check carefully. (The shank diameter of the corresponding tool is indicated by red number.) Long hole Pilot hole [ ~45HRC^ When finishing only the hole bottom Tool dia. (mm) Details are mentioned on Page 3 : Stocked Items. □ : Stocked by specified distributor. Contact with our sales department.
Open the catalog to page 6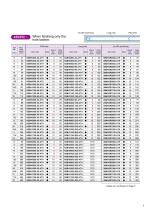
Long hole Tool dia. (mm)
Open the catalog to page 7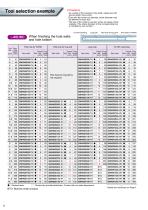
Tool selection ^Cautions •As a guide of the maximum hole depth, please set with groove length minus 2xDc. •Even with the same tool diameter, shank diameter may be different for each tool. •The size of the collet to use also varies, so please check carefully. (The shank diameter of the corresponding tool is indicated by red number.) When finishing the hole walls and hole bottom Tool dia. (mm) : Stocked Items. □ : Stocked by specified distributor. Contact with our sales department. ' y Details are mentioned on Page
Open the catalog to page 8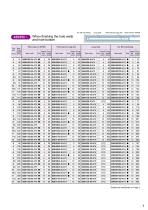
When finishing the hole walls and hole bottom Tool dia. (mm)
Open the catalog to page 9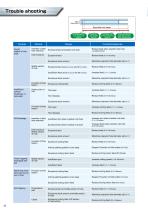
Trouble shooting insufficient surface
Open the catalog to page 10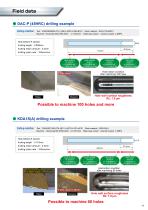
Field data ● DAC-P (45HRC) drilling example Cutting condition Tool:20WHSR0850-ATH(φ8.5×R201×L 256×φ10) Work material:DAC-P (45HRC) Machine:Horizontal MC (HSK-A63) vc=70m/min Water base coolant Internal coolant 2.2MPa Hole bottom R section Inching length:0.085mm Inching return amount:0.2mm Inching return rate:100mm/min Hole bottom R section Hole middle section Entrance section Pilot hole section Hole bottom condition after machining 100 holes Flank wear Hole wall surface roughness Rz: 1.5 µm Possible to machine 100 holes and more ● KDA1S(A) drilling example Cutting condition Hole bottom R section...
Open the catalog to page 11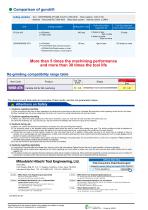
Culling condition Tool : 20WHSR0850-ATH (08.5xR2O1 *L256x010) Work material : DAC-P (A) Machine : Horizontal MC (HSK-A63) Water base coolant internal coolant 2.2MPa The diagrams and table data are examples of test results, and are not guaranteed values. A Attentions on Safety1. Cautions regarding handling (1) When removing the tool from its case (packaging), be careful that the tool does not pop out or is dropped. Be particularly careful regarding contact with the tool flutes. (2) When handling tools with sharp cutting flutes, be careful not to touch the cutting flutes directly with your bare...
Open the catalog to page 12All MOLDINO Tool Engineering Europe GmbH catalogs and technical brochures
 CUTTING TOOLS PRODUCTS CATALOGUE
1364 Pages
 CUTTING TOOLS PRODUCTS CATALOGUE
1056 Pages
 CBN-EPSB/CBN-EPSR
16 Pages
 EPBTS
12 Pages
 EMXR
16 Pages
 EMXA
12 Pages
 EPDRF-TH
12 Pages
 EPDBPE-ATH
20 Pages
 Epoch TH Power Mill
12 Pages
 Radius Precision ARPF
20 Pages
 Carbide Thread Mill series
16 Pages
 SCE-R
6 Pages
 RV type
12 Pages
 ABPFN type
6 Pages
 TD4N type
8 Pages
 EHHB-ATH
8 Pages
 EPCDS
4 Pages
 Epoch CFRP series
6 Pages
 EPSM-PN/ EPSW-PN
32 Pages
 GALLEA series
24 Pages
 WHMB-TH
12 Pages
 EMBE-ATH/EMBPE-ATH
16 Pages
 ETR(P)-TH,ETM(LN/P)-TH
16 Pages
 EPDRE-ATH
24 Pages
 CBN-EHB
12 Pages
 EHHBE-TH3
8 Pages
 TD6N type
12 Pages
 EB4HR-ATH
12 Pages
 EHX
12 Pages
 EPHB-PN
8 Pages
 EHHRE-TH3
8 Pages
 EDT
16 Pages
 EHSE-TH
8 Pages
 NSB
12 Pages
 WHNSB-TH
20 Pages
 EMSBS
8 Pages
 Ball Precision F ABPF type
16 Pages
 Radius Mill RD16B Type
8 Pages
 GS4TN type
4 Pages
 Red Screw Arbor
8 Pages
 ABP4F
8 Pages
 EPDBE-PN/ATH EPDSE-PN/ATH
32 Pages
 EPDBEH-TH3
20 Pages
 MINIATURE DRILL WHMB
8 Pages
 Epoch ® Combination Rib Ball
8 Pages
 PRODUCTS CATALOGUE 2015 - 2016
1070 Pages
 Carbide Non Step Borer series
28 Pages
 Drills for High-hardness Steels
16 Pages
 Face Mill : ASF type
8 Pages
 Face Mill : AFE45 type
8 Pages
 Ball Precision F : ABPF type
16 Pages
 Ball End Mill : ASB type
8 Pages
 Radius Precision : ARPF type
12 Pages
 Polish Mill V Type : ASPV Type
20 Pages
 Roughing End Mill : AME Type
12 Pages
 Radius Mill : AR type
20 Pages
 JM4060
4 Pages
 Epoch Micro?End Mill TH : EMM-TH
24 Pages
 Epoch Deep Radius Evolution
24 Pages
 Epoch Deep Ball Evolution Hard
16 Pages
 Epoch Micro Drill?EMD
24 Pages
 Radius Mill : ASR type
20 Pages
 Super Excellent MINI : ASM type
12 Pages
 Epoch "Mirus" Series
12 Pages
 Epoch G Turbo
8 Pages
 Roughing End Mill AME Type
12 Pages
 Z Plunging Borer?ZPB-TH
4 Pages
 Face Mill AFE45
8 Pages
 Epoch Micro Step Borer S
8 Pages











Archived catalogs
 Epoch CBN End Mill series
16 Pages
 HX3505 & HX3515
6 Pages
 GX2140
4 Pages
 Epoch "Panacea"
16 Pages
 Epoch Deep Evolution series
24 Pages
 Epoch SUS End Mill series
32 Pages
 Epoch Pencil Deep Ball Evolution
20 Pages
 Epoch Deep Radius F
12 Pages
 Re-grinding & Re-coating
20 Pages
 2009-2010 New Products Guide
5 Pages
 Micro Series for Micro Machining
14 Pages
 Milling Inserts
16 Pages
 Indexable Tools
160 Pages
 Threading Tools
6 Pages
 Turning Inserts
44 Pages
 HSS End Mills
98 Pages
 Reamers
16 Pages
 Cutters
10 Pages
 CBN End Mills
20 Pages
 Surface Treatment Tribec
8 Pages
 HSS Non Step Borer
36 Pages
 Carbide End Mills
280 Pages


- Milling tool
- Chuck
- Solid milling cutter
- Drilling tool
- Steel milling cutter
- Milling tool with replaceable insert
- Solid drill bit
- Metal milling cutter
- Clamping milling cutter
- Milling cutter with cylindrical shank
- End mill
- Cast iron milling cutter
- Face milling cutter
- Shell-end milling cutter
- Indexable insert milling cutter
- Ball nose milling cutter
- Cutting milling cutter
- Corner radius milling cutter
- Coated milling cutter
- High-performance milling cutter