
- Catalogs
- Fixtureworks
- Machinable Collet Clamps

- Company
- Products
- Catalogs
- News & Trends
- Exhibitions
Machinable Collet Clamps
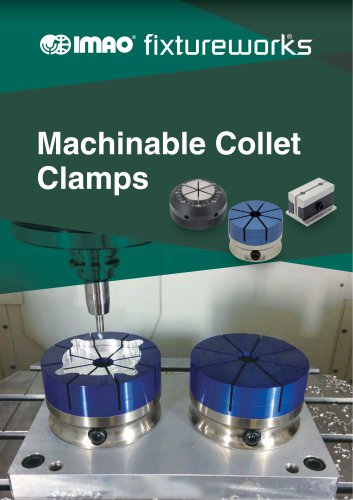
Machinable Collet Clamps
- Workpiece locating repeatability: ±0.03
- Jaw locating repeatability: ±0.02
- Values are for reference only; remaining jaw thickness should consider machining load.
- Key components include Locking Ring, Locating Hole, Hex Socket Button Head Screw, Clamping Pin, and Tapered Screws.
- AMWFH-I Jaws are made from A7075 aluminum and anodized for durability.
- The body is made from SCM435 steel, quenched, tempered, and nickel-plated.
- Avoid actuating clamping without a workpiece to prevent damage.
- Jaw Mounting: Fix clamping pin with the button head screw, supply air to the unclamping port, and mount the jaw by inserting the round pin into the locating hole.
- Jaw Machining: Machine the jaw to the workpiece contours within the machinable range.
- Workpiece Loading: Supply air to the unclamping port, load the workpiece, and supply air to the turbo port to clamp.
- Clamping force varies with air pressure, with a performance curve provided for reference.
- Ensure the locking ring is securely set at the bottom of the hole in the jaw.
- Press the jaw until the ground surface of the module is covered.
- Pricing, ordering, and CAD downloads are available at fixtureworks.com.
- Refer to the AMWFH-WP datasheet for mounting instructions of the Clamping Module.
Catalog excerpts
€&hmo’ fixture works Machinable Collet
Open the catalog to page 1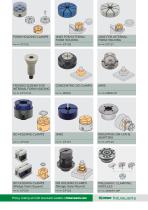
JAWS FOR EXTERNAL FORM HOLDING JAWS FOR INTERNAL FORM HOLDING TAPERED SCREWS FOR INTERNAL FORM HOLDING OD HOLDING CLAMPS (Wedge Style/Square) Part No. CPI 24 OD HOLDING CLAMPS (Wedge Style/Round) PNEUMATIC CLAMPING MODULES Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 2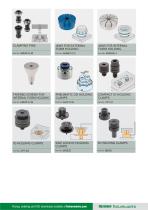
JAWS FOR EXTERNAL FORM HOLDING JAWS FOR INTERNAL FORM HOLDING TAPERED SCREWS FOR INTERNAL FORM HOLDING PNEUMATIC OD HOLDING CLAMPS_ SIDE LOCK ID HOLDING CLAMPS Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 3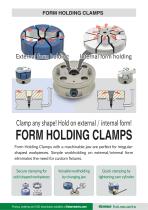
FORM HOLDING CLAMPS Clamp any shape! Hold on external / internal form! Form Holding Clamps with a machinable jaw are perfect for irregularshaped workpieces. Simple workholding on external/internal form eliminates the need for custom fixtures. Secure clamping for odd shaped workpieces Versatile workholding by changing jaw Quick clamping by tightening cam cylinder ^imno' fixture uu orks Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 4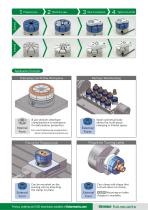
8 jaw sections distribute clamping force to workpiece for deformation prevention. Small cylindrical body allows the multi-piece clamping in limited space. Can be mounted on the existing vise by attaching the clamp on plate. External ICP122|Mounting-on-lathe Form Adapter is available. fixture works Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 5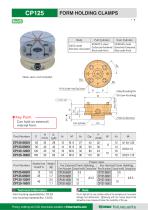
FOR M HOLDING CLAMP S RmUC ★Key Point - Can hold on external/ internal form. Part Number Part Number Technical Information Note ■Part locating repeatability: ±0.03 Do not tighten the cam cylinder without the workpiece set to prevent ■Jaw locating repeatability: ±0.02 damage and deformation. Tightening with the torque beyond the allowable screw torque will lower the durability of the jaw. Pricing, ordering and CAD downloads available at fixtureworks.com ^DifTMO' fixture works
Open the catalog to page 6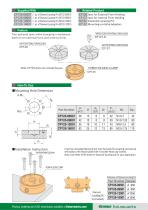
Related Product CPI 26|Jaws for External Form Holding CPI 27|Jaws for Internal Form Holding BJ7221 Diamond Locating Pin CPI 221 Mounting-on-lathe Adapters Supplied With ■ICP125-065011 :1 pc. of Diamond Locating Pin (BJ722-06001) ■ICP125-090011 :1 pc. of Diamond Locating Pin (BJ722-08001) ■ICP125-120011 :1 pc. of Diamond Locating Pin (BJ722-10001) ■ICP125-160011 :1 pc. of Diamond Locating Pin (BJ722-12001) ■ Mounting Hole Dimension ■ Installation Instruction Insert an included diamond pin into the body for locating and secure the body to the fixture plate with 4 socket-head cap screws. Note: Use...
Open the catalog to page 7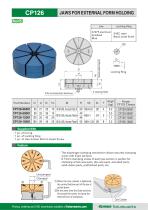
JAWS FOR EXTERNAL FORM HOLDING «r/11J Locking Ring Supplied With ■ 1 pc. of O-ring ■ 1 pc. of Hex Socket Button Head Screw ■ The diaphragm clamping mechanism allows securely clamping a part with 8 jaw sections. ■ 0.15mm clamping stroke of each jaw section is perfect for clamping of lost-wax parts, die-cast parts, extruded parts, solid-drawn parts, prefinished parts, etc. ©When the cam cylinder is tightened, the central bottom part of the jaw is pulled down. ©At the same time the 8 jaw sections tilt toward the center to clamp the external form of workpiece. Pricing, ordering and CAD downloads...
Open the catalog to page 8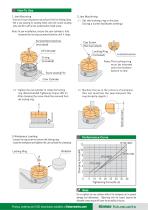
■ Insert an 0-ring to the groove on top surface of the Form Holding Clamp. 2-i. Set the locking ring in the jaw. ■Set a Jaw putting its locating holes onto the round locating (Using a screw facilitates setting.) pins and fix it with a hex socket button head screw. Note: At jaw installation, ensure the cam cylinder is fully loosened by turning counterclockwise until it stops. 2-2. -Tighten the cam cylinder to clamp the locking ring. (Recommended Tightening Torque:15N■ m) ■After clamping the screw should be removed from the locking ring. 2-3. Machine the jaw to the contours of workpiece. (Do not...
Open the catalog to page 9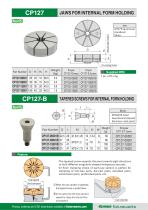
JAWS FOR INTERNAL FORM HOLDING Part Number CP127-B TAPERED SCREWS FOR INTERNAL FORM HOLDING SCM435 steel Quenched and tempered Electroless nickel plated ■The tapered screw expands the jaws towards eight directions to hold different irregularly-shaped workpieces securely. ■0.15mm clamping stroke of each jaw section is perfect for clamping of lost-wax parts, die-cast parts, extruded parts, solid-drawn parts, prefinished parts, etc. Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 10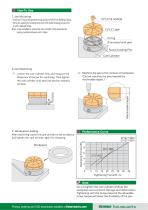
■ Insert an 0-ring to the groove on top surface of the Form Holding Clamp. ■ Set a Jaw putting its locating holes onto the round locating pins and fix it with a tapered screw. Note: At jaw installation, ensure the cam cylinder is fully loosened by turning counterclockwise until it stops. 2-1. Loosen the cam cylinder fully and measure the dimension of the jaw for machining. Then tighten the cam cylinder until each jaw section expands 0.15mm. 2-2. Machine the jaw to the contours of workpiece. (Do not machine the jaws beyond the machinable depth.) Performance Curve After machining loosen the cam...
Open the catalog to page 11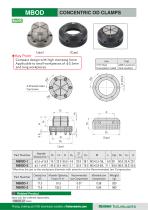
CONCENTRIC O D CLAMP S RrmjJC Compact design with high clamping force Applicable to small workpieces of 02.5mm and long workpieces_ Part Number *)Machine the jaw to the workpiece diameter with attention to the Recommended Jaw Compression. Part Number Related Product Jaws can be ordered separately. ■IMBOD-Oll Jaws Pricing, ordering and CAD downloads available at fixtureworks.com fixture works
Open the catalog to page 12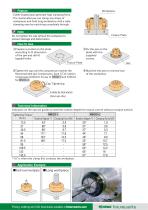
Feature ■Collet-shaped jaws generate high clamping force. ■The machinable jaw can clamp any shape of workpieces and hold long workpieces with a wide clamping area by machining completely through. Do not tighten the cap without the workpiece to prevent damage and deformation. ©Prepare a pocket on the plate according to D dimension of the jaw and drill 6 tapped holes. ©Tighten the cap until the compression reaches the Recommended Jaw Compression. Each 15°of rotation compresses 0.025mm for jaw of IMBOD-Il and 0.05mm ©Machine the jaw to nominal size of the workpiece. Technical Information Indicators...
Open the catalog to page 13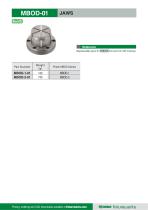
Replaceable iaws forlMBOD Concentric OD Clamps fixture works Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 14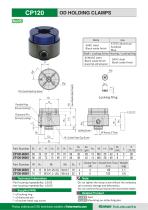
Locking Ring Diamond Pin (for body locating)" Part Number Part Number Technical Information / Note ■Do not tighten the clamp screw without the workpiece set to prevent damage and deformation. ■ Do not machine the jaw beyond the machinable depth. ■Part locating repeatability: ±0.03 ■Jaw locating repeatability: ±0.02 Pricing, ordering and CAD downloads available at fixtureworks.com
Open the catalog to page 15All Fixtureworks catalogs and technical brochures
 Quick Release Bail Lock Pins.
46 Pages
 Rollers and Bumpers.
50 Pages
 Pneumatic Clamps
45 Pages
 Bearing Guide Rollers
35 Pages
 Mechanical Linear Units
49 Pages
 5-Axis Clamping System
14 Pages
 Quick Shaft Clamps
15 Pages
 Torque Limiting Knobs & Handles
16 Pages
 Pneumatic Clamping Fasteners
14 Pages
 Modular Pull Clamping System
35 Pages
 Nutrunner Clamps
24 Pages
 Pneumatic Flex Locators
23 Pages
 Sliding Locks
41 Pages
 Work Supports
24 Pages
 Flex Locators
41 Pages
 Spring Clamps
24 Pages
 Side Clamps
27 Pages
 One Touch Fasteners
138 Pages
 One Touch Clamps
68 Pages
Archived catalogs
 QCTH / QCTHL / QCTHH
4 Pages
 QCSL
4 Pages
 QSC
2 Pages
 QCPC
4 Pages
 QCTH-N / QCTH-B
2 Pages
 Fixtureworks catalog
572 Pages
 KNOBS
27 Pages
 SPRING & BALL PLUNGERS
16 Pages
 TRIMAX VISES
40 Pages
 BUMPERS
14 Pages
 CMM_Inspection
10 Pages
 ROLLERS
30 Pages
 INDEXING PLUNGERS
13 Pages
 ADJUSTABLE HANDLES & LEVERS
37 Pages
 QUICK RELEASE BALL LOCK PINS
62 Pages
 CLAMPS
72 Pages
 Pull Handles
9 Pages
 MACHINE ACCESSORIES
8 Pages
 HAND WHEELS & CRANK HANDLES
25 Pages


