
- Catalogs
- Dapra Milling Solutions
- RHINO-FEED™ High-Feed Milling Series
RHINO-FEED™ High-Feed Milling Series

RHINO-FEED™ High-Feed Milling Series
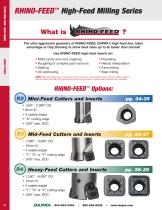
The RHINO-FEED™ series by Dapra is engineered for high-feed milling, enabling feed rates up to five times faster than standard rates. It is applicable for mold cavity and core roughing, complex part contouring, slotting, 2D contouring, pocketing, helical interpolation, face milling, and step milling. A strong air blast is recommended to manage heat due to high production rates.
- Mini-Feed Cutters: .500” - 2.000” OD, 8mm IC, 3 usable edges, “D” cutting edge, .030” max. DOC.
- Mid-Feed Cutters: 1.000” - 3.000” OD, 10mm IC, 4 usable edges, “T,” “D” or “F” cutting edge, .045” max. DOC.
- Heavy-Feed Cutters: 1.250” - 6.000” OD, 12mm IC, 4 usable edges, “T,” “D” or “F” cutting edge, .060” max. DOC.
This process involves significant chip thinning due to an extreme lead angle, requiring adjusted feed rates for maximum productivity. It allows for high feeds (IPM) but at lighter depths of cut (DOC). Specific instructions for each insert size optimize performance.
- Cutter Bodies: Made from through-hardened, extra-tough tool steel, surface hardened for wear resistance, and machined after hardening for excellent runout. Available in standard and long-reach bodies.
- Inserts: Designed for high feed rates in all materials, offering positive clearance for ramping and helixing capabilities. Multiple geometries are available for smooth cutting or strong edge conditions.
- Mini-Feed Inserts: Use a combination of feed and DOC based on the insert's capabilities. Compensated FPT recommendations are provided for optimal performance.
- Mid-Feed Inserts: Suitable for lighter-duty machines, with recommendations for feed and DOC adjustments based on the application.
- Heavy-Feed Inserts: Best for heavier DOC and larger machines, with specific FPT recommendations for different cutting conditions.
- Insert Grades: Various grades are available for different applications, with descriptions provided on page 40.
- Spare Parts & Tools: Information available on page 41.
- Application Information: Detailed guidance provided on page 41.
- Hole Diameter Calculation for Helical Interpolation: Instructions on page 42.
- Recommended Cutting Speeds: Available on page 43.
1. DMK15: Highest wear resistance, suitable for stable conditions across various materials. Variants include DMK15-TCI, DMK15-GLH, DMK15-TS, and DMK15-HM.
2. DMK30: Offers moderate wear and high shock resistance, ideal for interrupted or unstable steel applications. Variants include DMK30-TCI, DMK30-GLH, DMK30-TS, and DMK30-HM.
3. DMK35: Specially formulated for high-temperature alloys and austenitic stainless steels, with variants DMK35-HM and DMK35-IN.
4. DMK25: Provides higher wear resistance and good shock resistance, suitable for tough stainless steels and high-temperature alloys. Variants include DMK25-GLH and DMK25-HM.
5. DMP25: High wear resistance with moderate shock resistance, recommended for steel and ductile iron applications. Variants include DMP25-TCI, DMP25-GLH, DMP25-TS, and DMP25-HM.
- RHINO-FEED inserts are best for "Z-level" roughing and ramping, not solid plunging.
- Climb milling is required to prevent damage.
- Maintain 75% cutter diameter on the workpiece for optimal tool life.
- Use Feed Rate Compensation charts for optimal metal removal rates.
- Use anti-seize compound on screws and change insert screws every 10 inserts.
- Use the shortest tool holder for maximum rigidity.
- Clean pocket and screw at each insert change.
- Allows for larger diameter hole making using RHINO-FEED Cutters with helical interpolation.
- Maximum hole diameter is twice the tool diameter, but staying slightly under is recommended.
- Suggested operating parameters depend on material and tool conditions.
- Coatings like -TCI and -TS are suited for low-to-medium speeds, while -GLH and -HM are for high speeds and harder materials.
- Universal modular extensions are available for various head sizes, providing enhanced vibration dampening and rigidity.
- Options include carbide core and heavy-metal extensions for different applications.
The document describes Dapra's torque wrench system designed for secure and accurate insert loading and clamping. It highlights the advantages of the system, including enhanced grip and leverage compared to traditional wrenches, and offers two handle styles for user preference.
- TORX® Bits: Available in sets of 6 for sizes T10, T15, and T20, with corresponding product codes TW-BT-10, TW-BT-15, and TW-BT-20.
- Torque Drivers: Two styles are available: Straight-Handle (TW-SH-L) and T-Handle (TW-TH).
- Torque Adapters: Available for T10 (TW-AD-10), T15 (TW-AD-15), and T20 (TW-AD-20).
- Color-coded adapters and bits for easy identification.
- Preset torque values for each adapter size ensure accurate torque application.
- Audible 'CLICK' indicates when the correct torque is achieved.
Catalog excerpts
RHINO-FEED ™ HIGH-FEED MILLS RHINO-FEED ™ High-Feed Milling Series FEED What is The ultra-aggressive geometry of RHINO-FEED, DAPRA’s high-feed line, takes advantage of chip thinning to allow feed rates up to 5x faster than normal! Use RHINO-FEED high-feed inserts for: SINGLE-SIDED • old cavity and core roughing M • oughing of complex part contours R • Slotting • 2D contouring • Pocketing • Helical interpolation •FEED F ace milling • Step milling NOTE: High-feed milling does a tremendous amount of work in a short period of time. This line's high production rate can create more heat than typical milling tools. Strong air blast is recommended (multiple lines if possible). RHINO-FEED ™ Options: R2 Mini-Feed Cutters and Inserts • • • • • .500” - 2.000” OD 8mm IC 3 usable edges “D” cutting edge .030” max. DOC R3 Mid-Feed Cutters and Inserts • • • • • 1.000” - 3.000” OD 10mm IC 4 usable edges “T,” “D” or “F” cutting edge .045” max. DOC R4 Heavy-Feed Cutters and Inserts • • • • • 32
Open the catalog to page 1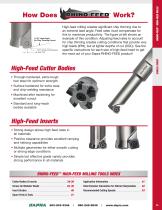
.010” actual chip thickness At .050” FPT High-feed milling creates significant chip thinning due to an extreme lead angle. Feed rates must compensate for FEED this to maximize productivity. The figure at left shows an example of this condition. Adjusting feed rates to account for chip thinning creates cutting conditions that provide very high feeds (IPM), but at lighter depths of cut (DOC). See the specific instructionsFEED of high-feed insert to get for each size the most out of your Dapra RHINO-FEED product! 11.50° Lead Angle (5x Chip Thinning Factor) RHINO-FEED ™ HIGH-FEED MILLS High-Feed...
Open the catalog to page 2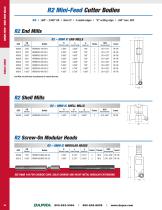
RHINO-FEED ™ HIGH-FEED MILLS R2 Mini-Feed Cutter Bodies R2 • .500” - 2.000” OD • 8mm IC • 3 usable edges • “D” cutting edge • .030” max. DOC Effective Length Overall Length End Mills are solid steel, manufactured for coolant thru tool. Effective Length R2 Screw-On Modular Heads R2 – 8MM IC MODULAR HEADS EDP Effective Length Overall Length Flutes Thread
Open the catalog to page 3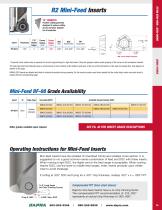
“D” INSERTS Positive cutting geometry designed to reduce cutting forces and heat. Suitable for all materials. T Corner Radius Corner Radius RHINO-FEED ™ HIGH-FEED MILLS * A special corner radius value is required for correct programming of a high-feed insert. Using the program radius avoids gouging of the corners in the workpiece material. The high-feed insert will naturally leave a small amount of extra material at the bottom-most layer of the cut, at the intersection of the wall and pocket floor. See diagram at bottom of this page. RHINO-FEED inserts are labeled with dots to indicate die position...
Open the catalog to page 4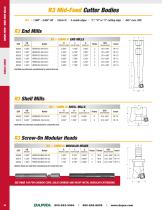
RHINO-FEED ™ HIGH-FEED MILLS R3 Mid-Feed Cutter Bodies R3 • 1.000” - 3.000” OD • 10mm IC • 4 usable edges • “T,” “D” or “F” cutting edge • .045” max. DOC Effective Length Overall Length End Mills are solid steel, manufactured for coolant thru tool. Effective Length Shell Mills are solid steel, manufactured for coolant thru tool. R3 Screw-On Modular Heads R3 – 10MM IC MODULAR HEADS EDP Effective Length Overall Length Flutes Thread Modular Heads are solid steel, manufactured for coolant thru tool
Open the catalog to page 5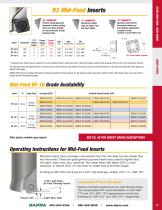
Left right: T, T, D Left to to right: N, N, D (Available in grade DMK30 only). Corner Radius Corner Radius “F” INSERTS Specially reinforced for the heaviest feeds and most abusive applications in steels or irons. “T” INSERTS Reinforced cutting edge for steels, irons and hard milling. .105” Corner Radius (Program) .190” * A special corner radius value is required for correct programming of a high-feed insert. Using the program radius avoids gouging of the corners in the workpiece material. The high-feed insert will naturally leave a small amount of extra material at the bottom-most layer of the...
Open the catalog to page 6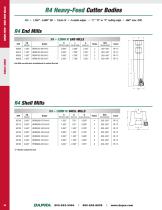
RHINO-FEED ™ HIGH-FEED MILLS R4 Heavy-Feed Cutter Bodies R4 • 1.250” - 6.000” OD • 12mm IC • 4 usable edges • “T,” “D” or “F” cutting edge • .060” max. DOC Effective Length Overall Length End Mills are solid steel, manufactured for coolant thru tool. Effective Length
Open the catalog to page 7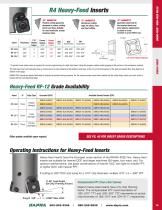
Left right: T, T, D Left to to right: N, N, D “F” INSERTS Specially reinforced for the heaviest feeds and most abusive applications in steels or irons. “T” INSERTS Reinforced cutting edge for steels, irons and hard milling. (Available in grade DMK30 only). Corner Radius Corner Radius .135” Corner Radius (Program) .220” * A special corner radius value is required for correct programming of a high-feed insert. Using the program radius avoids gouging of the corners in the workpiece material. The high-feed insert will naturally leave a small amount of extra material at the bottom-most layer of the...
Open the catalog to page 8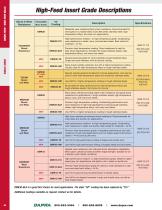
RHINO-FEED ™ HIGH-FEED MILLS High-Feed Insert Grade Descriptions Shock & Wear Resistance Uncoated (Base Grade) Moderate wear resistance/high shock resistance. Recommended for interrupted or unstable steel, most 300 series stainless steel, hightemperature alloys, and cast iron applications. High-performance medium- to high-temperature grade. Outstanding wear resistance in steels, irons, and stainless steels. Best suited for materials < 44 Rc. Premium high-temperature coating. Good resistance to heat for high-shock applications. Excellent for tough stainless steels, hightemperature alloys, and...
Open the catalog to page 9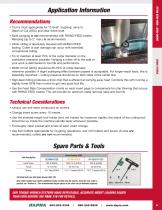
RHINO-FEED ™ HIGH-FEED MILLS Application Information Recommendations • ool is most appropriate for “Z-level” roughing; ramp to T Depth of Cut (DOC) and clear entire level. • olid plunging is not recommended with RHINO-FEED inserts. S Ramping (up to 2° max.) is recommended. • ry to maintain at least 75% of the cutter diameter on the T workpiece whenever possible. Hanging a cutter off to the side of your work is detrimental to tool life and performance. • idth of Cut (WOC) should be 60-75% of cutter diameter W whenever possible. A slight scalloping effect between passes is acceptable. For longer-reach...
Open the catalog to page 10All Dapra Milling Solutions catalogs and technical brochures
 Single-Sided Toroid Series
23 Pages
 High Feed Indexable Milling
12 Pages
 EXTREMEMetal Removal
25 Pages


