- Catalogs
- CHAIN HEADWAY
- HCM/ACM/SCM

HCM/ACM/SCM

HCM/ACM/SCM
Overview
This document provides a comprehensive technical guide for the HCM/ACM/SC St SRA Milling Cutter Series, designed for high-speed, precision milling in sectors such as aerospace, automotive, mold making, and electronics. It highlights advanced cutting edge technologies, dynamic balancing, and cooling systems to optimize performance and tool longevity.
1. Product Specifications
- Speed Capability: Cutters support spindle speeds up to 33,000 rpm for smaller diameters, with speed decreasing as diameter increases.
- Material Compatibility: Suitable for aluminum, copper alloys, plastics, carbon fiber reinforced composites, and other industrial materials.
- Insert Types: Utilizes polycrystalline diamond (PCD) and single crystal diamond inserts known for high hardness and wear resistance.
- Insert Seat Design: Precision-engineered seats ensure stable insert positioning and prevent detachment during high-speed rotation.
- Dynamic Balancing: Radial and axial adjustments reduce vibration and improve cutter stability.
- Through-Tool Coolant: Enhances chip evacuation and cooling, extending tool life and maintaining surface finish quality.
2. Cutter Models and Parameters
The series includes cutters ranging from 50 mm to 400 mm diameter, each with specified maximum spindle speeds and tooth counts. Examples include:
- HCM-50-FMB16-6T: 50 mm diameter, max 33,000 rpm, 6 teeth
- HCM-100-FMB32-14T: 100 mm diameter, max 29,500 rpm, 14 teeth
- HCM-400-FS60F-58T: 400 mm diameter, max 9,000 rpm, 58 teeth
Each model details spindle speed limits, tooth count, and weight for precise selection.
3. Insert and Seat Details
- PCD Inserts: Available in multiple geometries (45°, 73°, 75°) with optional wiper edges to enhance surface finish.
- Insert Seats: Interchangeable seats (e.g., ACM-SE12, ACM-AP16, ACM-RP12) tailored for different materials and cutting conditions.
- Adjustability: Micro-adjustments of insert edge height and position within 0.005 mm enable optimal cutting precision.
4. Cutting Technology and Recommendations
- Cutting Edge Angle: Recommended angles (e.g., 45°) balance chip thickness and cutting resistance to maximize tool life and surface quality.
- Engagement Ratio: Suggested cutting width engagement is 70-80% of cutter diameter, adjustable based on machine rigidity and workpiece characteristics.
- Force Components: Radial and axial cutting forces vary with edge angle; smaller angles favor axial force for long-length machining, larger angles favor radial force for thin-walled parts.
- Wiper Inserts: Should be installed 0.03-0.05 mm higher than PCD inserts to ensure proper surface finishing.
5. Material Cutting Conditions
- Recommended cutting speeds (Vc), feed rates (f), and depths of cut (Ap) are specified for materials such as aluminum alloys, copper alloys, plastics, graphite, and CFRP/GFRP.
- Examples: Aluminum alloys at Vc up to 700 m/min, Ap 1-2 mm; CFRP at Vc 100-300 m/min, Ap 0.1-0.4 mm.
6. Tool Assembly and Maintenance
- Balancing must comply with ISO 1940-1/8821 standards, especially for speeds above 10,000 rpm.
- Maximum spindle speeds must not be exceeded to avoid insert detachment and safety hazards.
- Torque specifications for screws and adjustment tools are provided to ensure correct assembly.
- Insert and wedge parallelism must be maintained with general accuracy of 0.01 mm and precision between 0.003-0.005 mm.
7. Accessories and Options
- Standard accessories include adjustment wedges, screws, torque drivers, and various insert holders.
- Interchangeable cartridges and insert seats allow customization for specific applications.
- Options for cutter bodies made from aluminum alloy, copper alloy, and alloy steel with anodized surfaces enhance rigidity.
Additional Technical Details
1. Product Identification and Components
Lists ACM and SCM series components such as aluminum changeable insert seats, converter keys, washers, water screws, and converter kits with detailed model numbers, dimensions, thread sizes, torque values, and weights.
2. Standard and Optional Accessories
Includes adjust screws, fixed screws, G-type rings, shims, PL-type wrenches for cutter height adjustment, cartridge fixing, and screw fastening. Optional accessories like spring pliers and assembly rings are also described.
3. Application Inserts and Cutting Conditions
Details inserts suitable for alloyed steels, stainless steels, cast irons, aluminum, refractory alloys, and hard materials. Inserts are classified by ISO standards and feature coatings such as ultra-micro, polycrystalline diamond, and ultra-hard microprogram coatings.
Cutting conditions specify speeds (Vc), feed per tooth (fz), and depth of cut (Ap) tailored to material type and hardness, differentiating continuous, general, and interrupted cutting.
4. Layer Coatings and Material Compatibility
Coatings like CHF, DP, and ultra-micro are matched to insert types and machining applications. Polycrystalline diamond coatings are emphasized for ultra-hard materials to optimize performance and tool life.
5. Cutting Parameters Tables
- Low-Alloy Steels: Speeds 180-300 m/min, feed 0.10-0.35 mm/rev, depth 0.5-3.0 mm.
- Stainless Steels: Speeds 80-160 m/min, feed 0.06-0.30 mm/rev, depth 0.5-3.0 mm.
- Cast Iron: Speeds 200-300 m/min, feed 0.06-0.30 mm/rev, depth 1.5-3.0 mm.
- Aluminum and Alloys: Speeds 400-1200 m/min, feed 0.05-0.30 mm/rev, depth 1.5-3.0 mm.
- Hard Materials (CBN, PCD): Speeds up to 2000 m/min, feed 0.04-0.10 mm/rev, shallow depths 0.05-0.50 mm.
6. Manufacturer and Contact Information
Contact details for Chain Headway Machine Tools Co., Ltd. are provided, including phone numbers, website, and social media for sales and technical support.
Critical Information and Best Practices
- Perform dynamic balancing adjustments for high-speed operation to minimize vibration and extend tool life.
- Use cutting parameters tailored to material and cutter size to optimize machining efficiency and surface finish.
- Install wiper inserts with the specified height offset relative to PCD inserts for optimal finishing.
- Maintain insert edge alignment and tool assembly precision regularly.
- Strictly adhere to maximum spindle speeds to prevent mechanical failure and ensure operator safety.
This document serves as an essential reference for selecting, assembling, and operating the HCM/ACM/SC St SRA Milling Cutter Series, ensuring high precision, efficiency, and safety in advanced milling applications.
Catalog excerpts
Milling Cutter Series
Open the catalog to page 1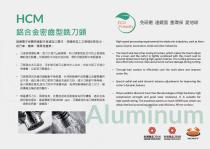
Ale SSA Siehc eR Lak 自 行 車 ・機 車・ 模 具 等 産業 ・ JB Riddists « AT Rie STAR : AE PINAR High-speed processing requirements for electronic industries, such as Aero- space, bicycle, locomotive, mold and other industries. The insert seat has a fine-tuning structure, which makes the insert adjust the p level, and the cutter is tightly combined with the, insert seat to prevent detachment during high-speed rotation. The cutting process can also effectively remove chips and prevent surface damage during cutting. coolant to efficiently cool the work-piece cutter life. FoR ASG) A Sho) MSP RRS - NASB PN ER Slee...
Open the catalog to page 3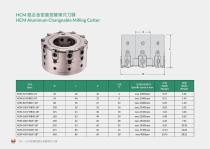
HCM Aluminum Changeable Milling Cutter
Open the catalog to page 4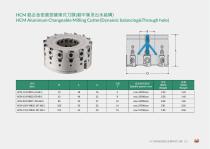
HCM 鍋 合 金 密 歯 型 替 換 式 刀 頭 ( 動 平衡 肥 出 水 結構 ) HCM Aluminum Changeable Milling Cutter(Dynamic balancing&Through hole)
Open the catalog to page 5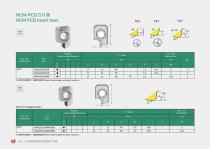
HCM-PCD刀 月 座 HCM PCD Insert Seat Polycrystalline Diamond If have the special angle need, please contact us. Ifhave the special angle need, please contact us.
Open the catalog to page 6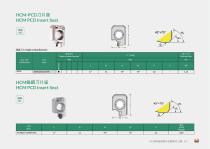
HCM-PCDJJFE& HCM PCD Insert Seat #8 7)F Single crystal diamond: Single crystal diamond
Open the catalog to page 7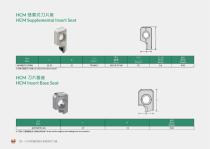
HCM ##2x AE HCM Supplemental Insert Seat ※ 可 自 行 搭 配 刀 月 材質 Can collocation insert material. JJHK#E Insert Base Seat 17 Can be used for weight or self-welding head of the material.
Open the catalog to page 8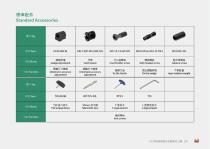
7) FEAR insert holder screw Sonat both headed screw T-type wrench L-type wrench
Open the catalog to page 9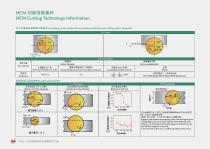
HCM 切削 技術 資料 HCM Cutting Technology Information hKLARERICH & 7S According to the width of the workpiece with the face milling cutter diameter 形式 Brie Part material E 建議 的 切 入 角 E The recommended cut-in angle 建議 刀 員 直 径 興 工 件 赴 度 比 Recommended tool diameterto workpiece width ratio eas a Choice suitable teeth 結果 Result SHABBY : 少 則 昌 起毛 下 More teeth easily deformed;less teeth easy to burr. Bite angle and tool life #9 Relation to Cutter Diameter Vf 一 と Relation to Cutter Position Relation to Tool Life 刀 Engage angle denotes the angle by which the full length of the "wa a cutting edge comes in contact...
Open the catalog to page 10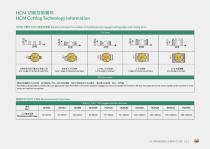
HCM 切削 技術 資料 HCM Cutting Technology Information TB Relation between the number of simultaneously engaged cutting edges and cutting force 形式 Re a HAY Bias OS1 時 0 or 1 edge in contact at same time. Bem LAB Only 1 edge in contact at any time. 2 edge in contact at any time. Normally, cutting width is considered to be appropriate with 70 to 80% of the cutter diameter engaged as shown in example D. However, this may not apply due to the actual rigidity of the machine or work piece, and machine horsepower. 建議 使用 刀 具 尽 寸 規 格 Recommended Cutter Spec. 71s Workpiece width range Suggest used the cutter...
Open the catalog to page 11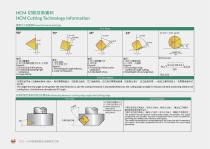
HCM 切削 技術 資料 HCM Cutting Technology Information 環 控 刀 月 座 種 類 Chose the insert seat type 90° Piers General: 1. Processing of thin pieces. 2. Processing clamping rigid workpiece. 3. Large cutting. | は ALS 2. Large cutting parts. General: 1. Processing of deep cavity workpiece. 2. In the depth of cut. number of rough cutting. 2. Small depth of cut, large feed. General: 1. Processing of rough embryos. The larger the chip angle is, the greater the chip thickness is, and the cutting resistance is increased.Otherwise, the cutting edge strength is reduced. General processing selection of cutting force,...
Open the catalog to page 12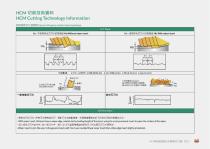
HCM Cutting Technology Information 如何 搭 配刀 月 座 類 型 How to Properly match insert seat type Hb : 使用 修 光 丸 刀 戸 的 粗糖 度 Hp: With wiper insert FA E3469) 7) Ae = Ha: Without wiper insert - With wiper insert: All insert have a wiper edge, relative to the beating height of the insert, using the most prominent insert to wiper the surface of the wiper.
Open the catalog to page 13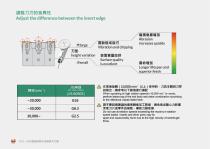
調整 刀 妨 的 差異 性 Adjust the difference between the insert edge BBaBiemM Abrasion fe S35 ALAR) Vibration and chipping increases quickly Surface quality Longer lifespan and superior finish RESULT RBCTBE When operating at high rotation speeds (10,000 min’ or more), perform balancing of the tool body and arbor combination according to the reference values listed here. Do not use at rotation speeds exceeding the maximum rotation speed stated. Inserts and other parts may fly apart and cause bodily harm due to the high velocity
Open the catalog to page 14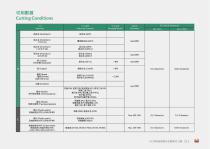
Materials examples
Open the catalog to page 15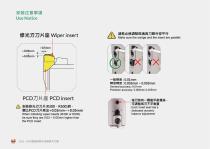
Make sure the wedge and the insert are parallel. When installing wiper inserts (R300 or R500) be sure they are 0.03 ~ 0.05mm higher than the PCD insert.
Open the catalog to page 16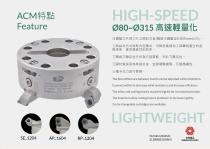
二 種 本 式 刀 座 可 替 換 The flute difference between inserts can be adjusted within 0.005mm. Covered within to decrease wind resistance and increase efficiency. The arbor and cutting head is mounted tightly for increased precision. The aluminum alloy cutting head is anod
Open the catalog to page 17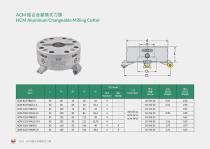
ACM 888 & Sia xt JGR HCM Aluminum Changeable Milling Cutter Insert Seat
Open the catalog to page 18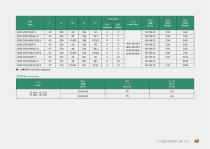
Insert Seat
Open the catalog to page 19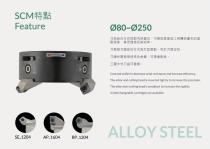
250 の 80の 刀 貞 結合 方 式 採取 内 包 覆 式 ・ 可 降 低 高速 加工 回 韓 時 産生 的 風 BRS EMS MRE 刀 具 興 刀 頭 定位 方 式 為 方 型 皿 配 ・ 利 於 刀 具 定位 力 頭 材質 採用 特殊 合金 鋼 ・ 可 提 高 剛性 ・ 三種 本式 刀 座 可共 換 ・ Covered within to decrease wind resistance and increase efficiency. The arbor and cutting head is mounted tightly to increase the
Open the catalog to page 20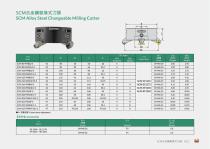
SCM 合 金 鋼 替 換 式 用 豆 SCM Alloy Steel Changeable Milling Cutter Insert Seat
Open the catalog to page 21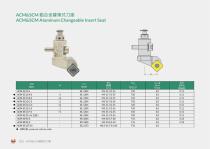
ACM&SCM #48 & Bihar ACM&SCM Aluminum Changeable Insert Seat @ - 2842 -produced order by order.
Open the catalog to page 22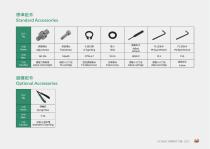
Adjust Screw Fixed Screw G-Type Ring PL-Type Wrench PL-Type Wrench Adjust cutter height Bless Bie Fix adjust screw Adjust cartridge HERS Fasten
Open the catalog to page 25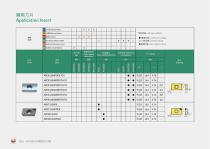
#21 FA 7) Application Insert Pll 2 + iS Alloyed Steels Refractory Alloys Hard Material BIRRRE Cutting Condition: O— tH General Cutting @ 2) A) Interrupted Cutting
Open the catalog to page 26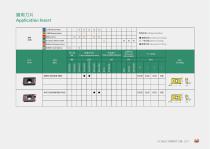
#21 FF Application Insert eM 218 Alloyed Steels iMG Stainless Steels K EE Cast Iron + HUHRE Cutting Condition: Interrupted Cutting Polycrystalline diamond Uitra-hard microprogram Continuous Cutting Refractory Alloys
Open the catalog to page 27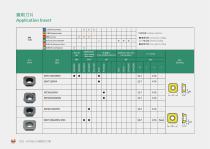
#21 FA) Fi Application Insert | Sif Alloyed Steels ‘*PMGiE Stainless Steels TD BIHKRS Cutting Condition: Refractory Alloys 18 ff Hard Material Layer coating
Open the catalog to page 28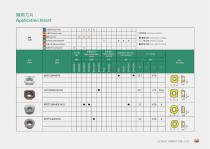
t) Bilik 6 Cutting Condition: Hard Material
Open the catalog to page 29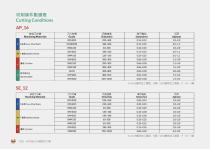
Cutting Conditions 被 加工 材質 Machining Materials S29) Low-Alloy Steels JARS Grade SERS fz(mm/rev) Cast Iron MLAS Machining Materials S28 Low-Alloy Steels FANT S82! : N38 | SCMii FADD
Open the catalog to page 30
Cutting Conditions SE 12 RIL Machining Materials Machining Materials A fifi Alloy Steels 7 $8 2 Stainless Steels (4 #238 Cast Iron Nh) 紹 合 金 Aluminum&Al
Open the catalog to page 31All CHAIN HEADWAY catalogs and technical brochures
 PCD & PCBN PRECISION INSERT
24 Pages
 STH&TPL Tapping holder Series
20 Pages
 Angle Head Series
24 Pages
 PNER Collet Chuck Series
20 Pages
 DP Anti Vibration Series
28 Pages
 SSP M405 Chamfering Series
16 Pages
 Mini End Mill Cutter Series
16 Pages
 CHAMFERING CUTTER SERIES
28 Pages
 SIDE MILLING CUTTER SERIES
24 Pages
 DEBURRING TOOL
2 Pages
 Turning Inserts
12 Pages
 VOL.7
853 Pages