
- Catalogs
- Bolte GmbH
- WELDING STUDS FOR DRAWN ARC STUD WELDING WITH CERAMIC FERRULE

- Products
- Catalogs
- News & Trends
- Exhibitions
WELDING STUDS FOR DRAWN ARC STUD WELDING WITH CERAMIC FERRULE

WELDING STUDS FOR DRAWN ARC STUD WELDING WITH CERAMIC FERRULE
This document outlines the technical specifications and guidelines for welding studs used in drawn arc stud welding with ceramic ferrules. It details the types of studs, materials, dimensions, surface treatments, and accessories.
The document begins by describing the use of a pressed-in aluminum ball at the welding tip to enhance ignition and arc stabilization, with exceptions for certain insulation pins and rectangular studs. Ceramic ferrules are standard for weld pool backing, though shielding gas is an alternative.
Welding studs are made from steel and stainless steel, adhering to DIN EN ISO 13918 and DIN EN ISO 14555 standards. Material properties are verifiable through inspection documents.
Dimensions are provided in tables, with nominal lengths corresponding to post-welding lengths. Special dimensions are available upon request.
Studs are typically supplied in a bright condition, with optional treatments like galvanic zinc plating and hot zinc dipping, which may affect welding quality and require mechanical removal from the welding tip.
Threads are cold rolled according to DIN 13-1 standards, with special threads available upon request.
A weld fillet forms during welding, with dimensions defined by the ceramic ferrule and welding parameters.
Accessories for stud welding guns must be adjusted to the welding element, with specific accessories listed in the document.
Shear connectors (types SD1 and SD3) conform to DIN EN ISO 13918 and meet EU construction product regulations, with European Technical Assessment (ETA) certification.
The document provides comprehensive specifications for various types of welding studs and accessories, ensuring compliance with international standards and offering customization options for specific requirements.
- Bimetallic Internally Threaded Stud (Type ID-DUO): Specifications available upon request.
- Insulation Pins and Clips: Various types with specific dimensions and materials, including optional ceramic ferrules for special applications.
- Rectangular Studs (Types A, B, C): Specifications include optional aluminum ball inclusion.
- Threaded Collar Stud (Type KRB) and Collar Stud (Type KRS): Dimensions and materials specified, with ceramic ferrule options.
- Threaded Stud (Type M): Various thread sizes and materials, with dimensions available upon request.
- Other Stud Types: Includes various specialized studs with dimensions and materials available upon request.
- Padded Ring for Shear Connectors: Guidelines for use with item numbers for different diameters.
- Dimensions and materials not listed are available upon request.
- Explanations for materials and surface treatments are in Chapter 1.1.
- Item numbers include placeholders (XXX) for specific welding element lengths.
Catalog excerpts

WELDING STUDS FOR DRAWN ARC STUD WELDING WITH CERAMIC FERRULE
Open the catalog to page 1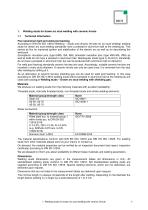
Welding studs for drawn arc stud welding with ceramic ferrule Technical information Flux (aluminium ball) and weld pool backing According to DIN EN ISO 13918 (Welding – Studs and ceramic ferrules for arc stud welding) welding studs for drawn arc stud welding standardly have a pressed-in aluminium ball at the welding tip. This serves as flux for improved ignition and stabilization of the electric arc as well as for deoxidising the weld pool. (Exceptions: Insulation pins (type ISMS, ISA, ISB), bimetallic insulation pins (type VBS-MS, VBS) as well as balls do not have a pressed-in aluminium ball....
Open the catalog to page 7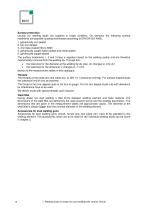
Surface protection Usually our welding studs are supplied in bright condition. On demand, the following surface treatments are possible (coating thicknesses according to DIN EN ISO 4042): 1. galvanically zinc-plated 2. hot zinc dipped 3. zinc flake coated flZnnc-600h 4. galvanically copper-base-coated and nickel-plated 5. galvanically copper-plated The surface treatments 1, 2 and 3 have a negative impact on the welding quality and are therefore mechanically removed from the welding tip. Through this: • the tolerance for the diameter at the welding tip (d2 resp. d1) changes to -0,6/+0,1 • the...
Open the catalog to page 8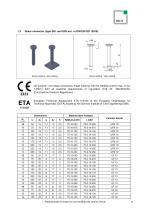
Shear connector (type SD1 and SD3 acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding CE-conform. Our shear connectors (head marking: SB (for S235J2+C470) resp. A (for 1.4301)) fulfil all essential requirements of regulation (EU) Nr. 305/2011/EU (Construction Products Regulation). European Technical Assessment ETA-11/0120 of the European Organisation for Technical Approvals (EOTA) issued by the German Institute of Civil Engineering (DIBt). Material (item number) Ceramic ferrule 1. Welding studs for drawn arc stud welding with ceramic ferrule
Open the catalog to page 9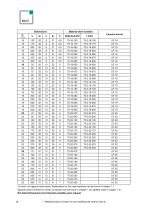
Material (item number) Ceramic ferrule *d3 and h are approximate values. Explanations to the used materials can be found in chapter 1.1. Special ceramic ferrules for shear connectors can be found in chapter 1.32, padded rings in chapter 1.31. Not listed dimensions and materials available upon request. 1. Welding studs for drawn arc stud welding with ceramic ferrule
Open the catalog to page 10
Threaded stud with reduced shaft (type RD acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding The threaded stud type RD is threaded almost to the top of the welding tip which is reduced to about the core diameter of the thread. Thus the fillet diameter will only be slightly (0,5-1 mm) bigger than the external diameter of the thread. It is worthy of note that the reduction of the welding tip diminishes the bearing force of the stud by approximately 15% in comparison to the type MD/PD/FD. Thus - if necessary - the next bigger diameter should be chosen. Dimensions...
Open the catalog to page 11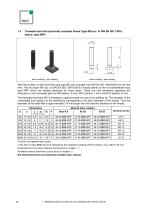
Threaded stud with practically complete thread (type MD acc. to DIN EN ISO 13918, before: type MPF) before welding / after welding before welding / after welding With the revision of April 2018 the stud type MD was included into DIN EN ISO 13918:2018 for the first time. The stud type MD acc. to DIN EN ISO 13918:2018 is mostly identic to the not standardised stud type MPF which we already produced for many years. There are only deviations regarding the dimension y (non-threaded part) for M6 (before: 3 mm), M10 (before: 7 mm) and M12 (before: 8 mm). The threaded stud type MD is threaded to approximately...
Open the catalog to page 12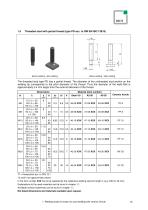
Threaded stud with partial thread (type PD acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding The threaded stud type PD has a partial thread. The diameter of the unthreaded stud section on the welding tip corresponds to the pitch diameter of the thread. Thus the diameter of the weld-fillet is approximately 3-4 mm larger than the external diameter of the thread. Dimensions d1 Material (item number) Ceramic ferrule = thread pitch acc. to DIN 13-1 *d3 and h are approximate values. In the item number XXX has to be replaced by the respective welding element length...
Open the catalog to page 13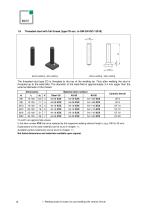
Threaded stud with full thread (type FD acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding The threaded stud type FD is threaded to the top of the welding tip. Thus after welding the stud is threaded up to the weld-fillet. The diameter of the weld-fillet is approximately 3-4 mm larger than the external diameter of the thread. Dimensions Material (item number) * *d3 and h are approximate values. In the item number XXX has to be replaced by the respective welding element length l 2 (e.g. 030 for 30 mm). Explanations to the used materials can be found in chapter...
Open the catalog to page 14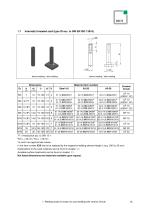
Internally threaded stud (type ID acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding Material (item number) d3* h* Ceramic ferrule = thread pitch acc. to DIN 13-1 l2 < 20 mm, 3for l2 < 25 mm *d3 and h are approximate values. In the item number XXX has to be replaced by the respective welding element length l 2 (e.g. 030 for 30 mm). Explanations to the used materials can be found in chapter 1.1. Available surface treatments can be found in chapter 1.1. Not listed dimensions and materials available upon request. 2for 1. Welding studs for drawn arc stud welding...
Open the catalog to page 15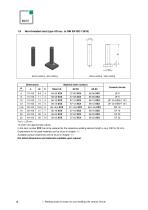
Non-threaded stud (type UD acc. to DIN EN ISO 13918) before welding / after welding before welding / after welding Material (item number) Ceramic ferrule l2 < 20 mm *d2 and h are approximate values. In the item number XXX has to be replaced by the respective welding element length l 2 (e.g. 030 for 30 mm). Explanations to the used materials can be found in chapter 1.1. Available surface treatments can be found in chapter 1.1. Not listed dimensions and materials available upon request. 1. Welding studs for drawn arc stud welding with ceramic ferrule
Open the catalog to page 16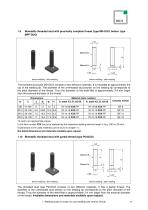
Bimetallic threaded stud with practically complete thread (type MD-DUO, before: type MPF-DUO) before welding / after welding before welding / after welding The threaded stud type MD-DUO consists of two different materials. It is threaded to approximately the top of the welding tip. The diameter of the unthreaded stud section on the welding tip corresponds to the pitch diameter of the thread. Thus the diameter of the weld-fillet is approximately 3-4 mm larger than the external diameter of the thread. Dimensions d1 Ceramic ferrule Material (item number) d3 * *d3 and h are approximate values. In...
Open the catalog to page 17All Bolte GmbH catalogs and technical brochures
 ZUBEHÖR ACCESSORIES
104 Pages
 PKA-500 PHA-500 PHA-500-6
4 Pages
 VBZ
4 Pages
 KKA-200F KHA-200F
4 Pages
 SERIES V
6 Pages
 SERIES T
6 Pages
 PIM-1B PIM-1K
4 Pages
 PKM-1B PHM-1A
4 Pages
 GD
6 Pages
 PHM
4 Pages
 LBS
6 Pages
 PRO-S
6 Pages
 PRO-I
8 Pages
 PRO-D
6 Pages
 SHEAR CONNECTORS
4 Pages
 BOLTE GmbH
6 Pages



- Welding system
- Automatic welding machine
- Welder
- Feeder
- Manual gun
- Arc welder
- Portable welder
- Arc welding machine
- Precision welding machine
- Inverter welder
- Automated feeder
- DC welder
- Automatic gun
- 230V single phase welding machine
- CNC welding machine
- Pneumatic sealer
- Pneumatic gun
- Benchtop welding machine
- Power adapter