
- Catalogs
- Alfamatic Srl
- PRESS-RIGHT

PRESS-RIGHT

PRESS-RIGHT
Press-Right is a device used for monitoring and measuring in production processes. It connects to a press, displacement transducer, and load cell to monitor positions and forces, ensuring quality by analyzing position-force curves.
Data on cylinder position and force is recorded to create a position-force graph. Consistent curves indicate quality, while deviations suggest issues.
The cycle includes stages like Approach, Contact, Work, Pre-arrest, Wait, and Return, each with specific speed and force parameters.
Absolute positions are from the cylinder's zero point, while relative positions are from the contact point. The device uses a force transducer to set these positions.
Monitoring involves a tolerance range for force and position. Deviations lead to piece rejection. Cylinder return is monitored by force or position values.
Refer to the manual for installation. Guidance is provided for setting up and operating the device, including practical tests.
The device features a menu for navigation. Users can perform manual movements to familiarize themselves with the machine.
Jobs consist of cylinder movement and curve control parameters. Users can create, manage, and edit jobs, setting parameters like final position and speeds.
Users can adjust the position-force graph settings, including origin and scale.
The device includes self-check functions and options for additional sensors for further control.
Details on force measurement within a height range, job options, and tolerance bands are provided. Rejected pieces require a reset to continue.
The Tools menu allows for device configuration, including display management and transducer calibration.
Diagnostic functions require qualified personnel. Special configurations include additional transducers and RFID tool recognition.
Checkpoints have parameters for force, position, and other values, stored in specific registers.
Issues are categorized with specific codes. Troubleshooting covers common problems and solutions.
Press-Right manages position-force curves, supports job management, and offers connectivity features. Proper recycling is required for disposal.
Catalog excerpts

PRESS-RIGHT FOR ELECTRIC PRESS • User manual
Open the catalog to page 1
1 General information Press-Right is a monitor and measuring device that is connected to a press and monitors the quality of productive processes. Being interfaced with a displacement transducer and a load cell, it continuously monitors its positions and instantaneous force. Notes on control theory During sample production, the data regarding cylinder position and the force exerted by it are entered; the following graph may be created: position-force representing production. If several runs are performed on similar pieces, their position-force curves will also be similar. On the other hand, if...
Open the catalog to page 5
1.2.3 Work The work can be performed in two ways depending on whether the pre-stop is used or not. The work without pre-stop is performed when the Pre-stop position is equal to zero. Work without pre-stop During work without pre-stop the cylinder advances at the Working speed until the stop value is reached. Once the stop value has been reached, the cylinder is stopped. Work with pre-stop During work with pre-stop the cylinder advances at the working speed until the Pre-stop position is reached. Once the Pre-stop value has been exceeded, the cylinder advances up to the stop value, correcting...
Open the catalog to page 6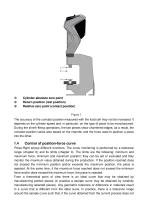
Cylinder absolute zero point Return position (rest position) Relative zero point (contact position) Figure 1 The accuracy of the conctact position measured with the load cell may not be increased. It depends on the cylinder speed and, in particular, on the type of piece to be manufactured. During the shrink-fitting operations, the two pieces show chamfered edges; as a result, the conctact position varies also based on the chamfer and the force used to position a piece into the other. Control of position-force curve Press-Right enjoys different functions. The curve monitoring is performed by a...
Open the catalog to page 7
stay inside such range, the piece is classified as scrap. The piece is good only if the analysis of the minimum/maximum limits and the tolerance range have a positive result. Press-Right also monitors the cylinder return at the end of the production process. Such return may result from the exertion of a specific force (stop force) or at a specific position (final position). It is possible to set both force and position stop values at the same time; in this case the first value to be entered will govern the cylinder return. By changing the value of the configuration, it is also possible to command...
Open the catalog to page 8
2 Installation of Press-Right For the installation of the device on the machine, please refer to the specific manual.
Open the catalog to page 9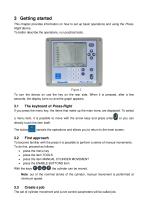
3 Getting started This chapter provides information on how to set up basic operations and using the PressRight device. To better describe the operations, run practical tests. Figure 2 To turn the device on use the key on the rear side. When it is pressed, after a few seconds, the display turns on and the graph appears. If you press the menu key, the items that make up the main menu are displayed. To select a menu item, it is possible to move with the arrow keys and press enter directly touch the item itself. The button cancels the operations and allows you to return to the main screen. First...
Open the catalog to page 10
To create a job: • press the menu key • press the Jobs management item • press the Create a new job item. • Enter the name that identifies the job (example TEST 1) and press the enter key. Note: in the rest of this manual, when it is indicated, for example, to select the command Jobs management > Create a new job, you intend to press the menu key then press the item Jobs management and finally press the item Create a new job. Once the work has been created, it is necessary to define how the cylinder should move. The motion profile parameters can be found in Edit job > Movement management. Before...
Open the catalog to page 11
The Show measured values item displays the values measured during the last cycle. The Tools allows the modification of the instrument configuration and the possibility to move the cylinder manually. The item Piece counter is used to reset the counter of processed pieces. The item Part number allows you to enter the identification number of the piece being processed. 3.6.1 The special functions of keys in the main menu displays the cursor to measure the force at a certain point on the curve. To move the cursor, use the arrow keys If menus are not displayed, press the windows showing the special...
Open the catalog to page 12
4 The JOB The Press-Right stores all the settings (parameters, band and counters) relating to the various jobs in an internal memory. Each group of settings is called “Job”. Each job has its own name. In the main menu there is the item Jobs management. Through this menu it is possible to choose a job among those present, create a new one, or delete the job in use. To create a new job, use the Jobs management > Create a new job command and give it a name. As a name you can use the number of the design, the name of the customer or whatever you prefer to be able to easily identify it. When you create...
Open the catalog to page 13
Each job has a piece counter. To access the counter options, select the Job management > Edit job > Scheduling menu. In this menu it is possible to reset the counter of the pieces or choose a maximum number of other pieces to block the instrument. Managing the automatic selection of jobs as an external user When the automatic job selection is activated, the Press-Right prepares the selectable jobs. These jobs are initially empty. To make an empty job usable, access the Job management> Change job menu and press enter on the desired job, at this point it will be possible to choose the name of the...
Open the catalog to page 14
To use more phases, it is necessary to enable the execution of the phases in the menu Job properties> PHASES MANAGEMENT> enable phases. With the keys it is possible to display the desired phase and modify its parameters with the MODIFY PHASE menu. The phases will be carried out automatically in sequence. If you want to perform one individually out of sequence, select the PHASE TO EXECUTE menu. A phase can be repeated several times. Channel management Up to six force transducers can be connected to the Press-Right to control as many displacement-force curves. While each force transducer detects...
Open the catalog to page 15All Alfamatic Srl catalogs and technical brochures
 ELECTRIC CYLINDERS
20 Pages
 Electric Presses Catalogue
32 Pages
 Air-Oil Booster
8 Pages
 Op Presses Catalogue
48 Pages

